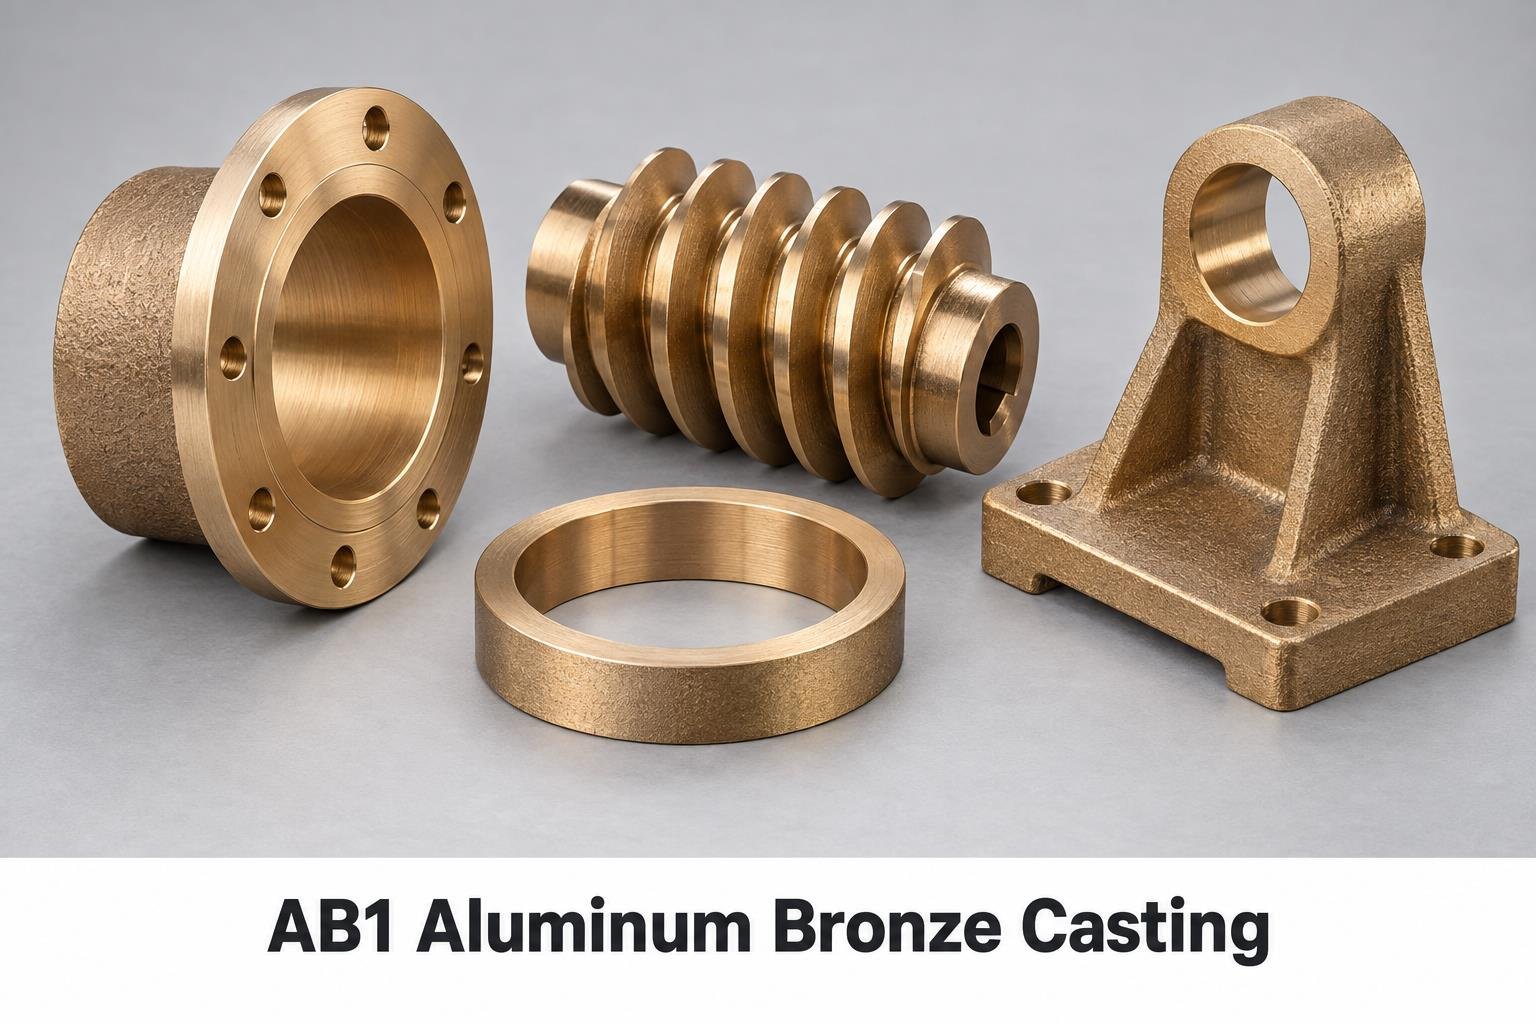
AB1 Aluminum Bronze Casting
Price: US$ 19.00/kg
AB1 Aluminum Bronze Casting from Brass Parts India covers drawing-controlled AB1 aluminum bronze components for wear, load-bearing and general corrosion-service duties. The specified material is AB1 / CuAl10Fe-type, a iron aluminum bronze grade supplied as drawing-based castings, rough-machined blanks or finish-machined components. Target buyers include electrical OEMs, EPC contractors, power utilities, pump and valve manufacturers, marine equipment builders and industrial distributors. Quote review connects alloy condition, casting route, section thickness, machining allowance, inspection and service environment. The listed product rate is US$ 19.00/kg; tooling, machining, testing, packing and freight are confirmed against the drawing and quantity.
The listed kilogram rate is the product reference price. Confirm chargeable weight, tooling, machining, finishing, testing, packing and delivery terms in the quotation.
Detailed product overview
| Grade designation | AB1 / CuAl10Fe-type |
|---|---|
| Material family | iron aluminum bronze |
| Chemistry basis | Copper-aluminum-iron bronze chemistry to the ordered AB1 or approved project specification |
| International references | AB1 legacy designation; CuAl10Fe-type family; related BS 1400 and EN 1982 grades must be compared clause by clause |
| Typical components | bushes, gears, wear plates, valve parts, guides, brackets and general engineering castings |
| Published rate | US$ 19.00/kg |
Material identity and purchasing designation
Aluminum bronze is a copper-based alloy family in which aluminum is the principal alloying addition. It is not an aluminum-base casting alloy. Iron and, for nickel aluminum bronze, nickel help define the grade. Select the material using the actual service loading, environment and required delivery condition. State the standard designation and required supply condition on both the enquiry and the purchase order. The description should remain consistent across the drawing, quotation, material certificate and inspection record. This avoids a technically different alloy being accepted because its commercial name sounds similar.
Wear rings and bearing sleeves
The correct bronze depends on the mating material, load, sliding speed, lubrication and operating clearance. Hardness alone does not establish suitability for a bearing. Specify the counterface and running diameter separately from the as-cast envelope. For hot equipment, differential expansion must be considered when setting cold clearances. Abrasive contamination, poor lubrication and misalignment require design controls rather than a simple alloy change.
Marine pump and valve components
Nickel aluminum bronze is considered for marine equipment, but seawater suitability depends on chemistry, microstructure, water conditions and contact with other metals. Mark the critical zones on pump bodies and impellers. State any metallographic examination, pressure testing, repair restrictions and specified heat treatment before production. The word marine is not a certification and does not define a universal corrosion life.
Heat treatment and machining sequence
Treatment requirements vary with grade and service specification. Agree the material condition before planning rough and finish machining. Rings, long bushes and thin flanges need allowance for distortion and datum recovery. A component with both a wear face and a pressure wall must preserve minimum section thickness after its final machining operations.
Key features and engineering requirements
- Drawing-defined ab1 aluminum bronze castings with an identified alloy specification.
- Process selection matched to geometry, cores, section thickness and order quantity.
- Defined machining stock for bores, threads, mounting faces and sealing interfaces.
- Inspection requirements linked to component function and critical zones.
- Material identification and documentation specified with the purchase order.
- Supply condition, surface finish and packing agreed before production.
Machining allowance and datum strategy
Machining stock must cover casting variation without adding unnecessary weight or cutting time. Define allowances by surface rather than applying one blanket value to the whole component. A bore and an external flange may need different allowances. Establish how the first machining operation locates the casting, then how subsequent operations preserve the datum relationship. For cored components, check minimum wall thickness after machining. Stock allowance is a process-design decision and should be agreed before the pattern or permanent tool is finalized.
Surface condition and defect acceptance
As-cast texture, gate-removal marks and parting lines differ from machined surface roughness. Identify visible areas, functional areas and surfaces that will be covered during assembly. Specify acceptable dressing and whether weld repair, impregnation or other corrective work is allowed. Inspection should distinguish harmless surface texture from defects affecting strength, leakage or fit. A reference sample can support an appearance requirement, but it should supplement measurable criteria and a documented agreement about critical surfaces and permissible repair.
Threads, fits and mating components
The finished component must fit the mating assembly, not merely match its own isolated dimensions. Specify thread standard, pitch, tolerance class and usable engagement length. State fit requirements for shafts, bushes and locating pins. Where a coating is applied, clarify whether dimensions are measured before or after finishing. Chamfers and edge breaks should support safe assembly without reducing sealing land or contact area. Provide the mating-part information needed to review tool access, assembly sequence and inspection-gauge selection.
Heat treatment and property verification
Heat treatment is grade-dependent and should be specified only where it is required by the alloy standard or component design. Define the delivery condition and associated testing rather than requesting a generic treatment for all copper alloys. A separately cast test coupon may not represent every local section of a complex component. Agree the sampling arrangement and any supplementary verification. Hardness, tensile properties, conductivity and metallography answer different questions and should be selected according to the function of the supplied casting.
Technical specifications
| Parameter | Purchasing requirement |
|---|---|
| Product category | Metal casting |
| Material family | aluminum bronze |
| Listed price | US$ 19.00/kg |
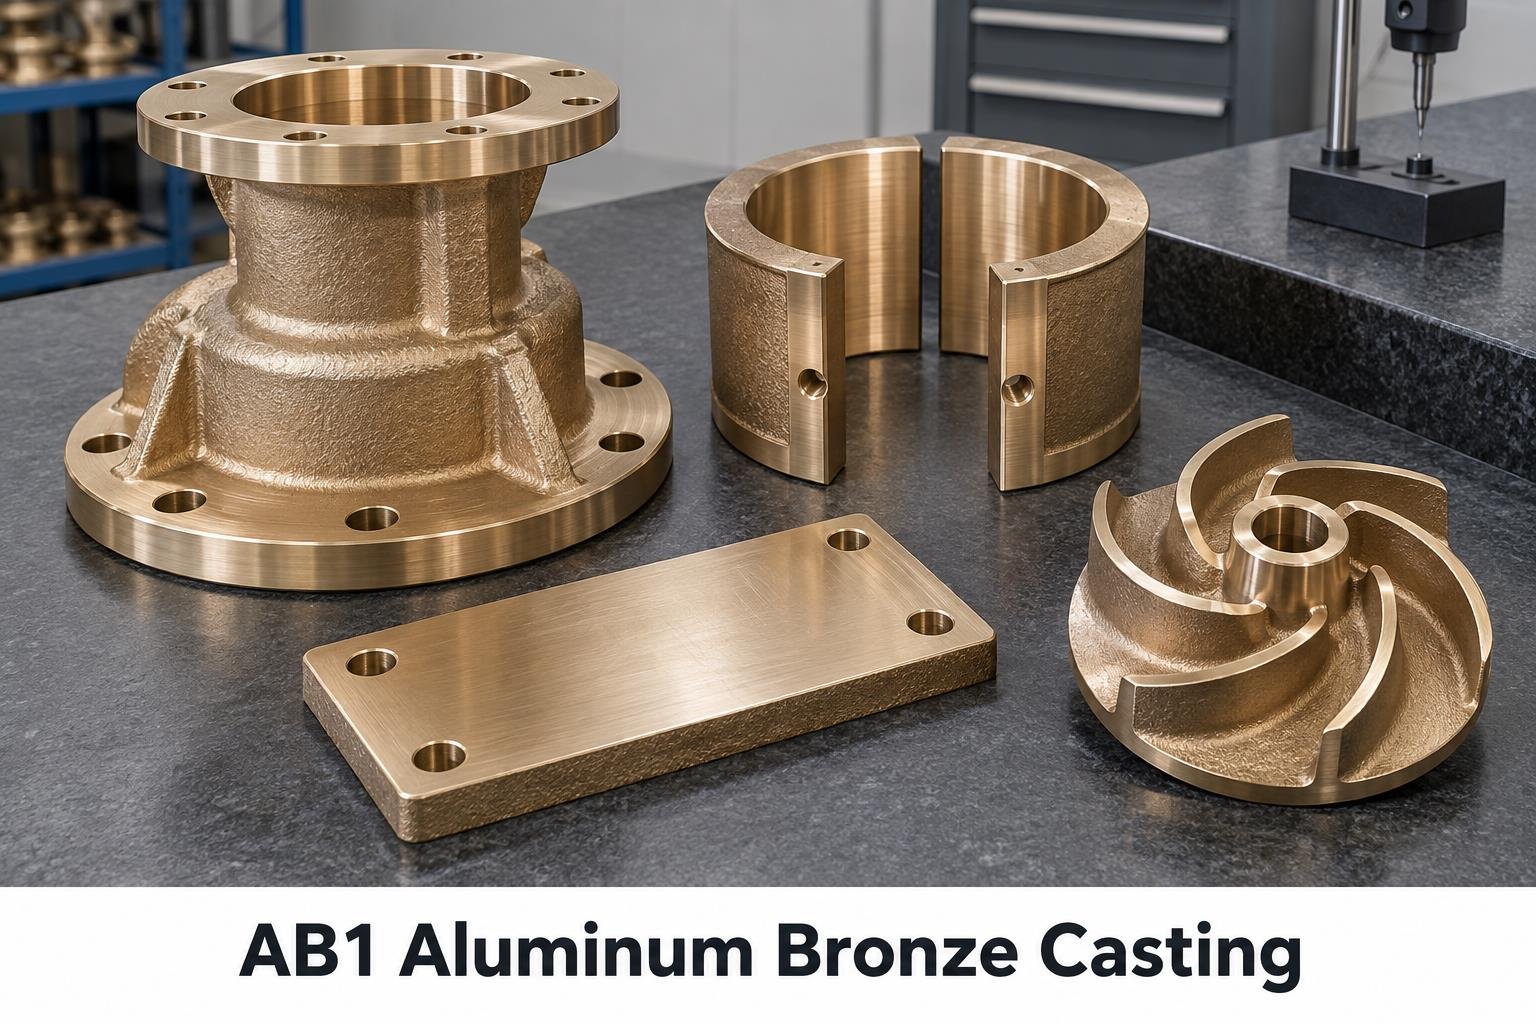
| Typical components | pump casings, impellers, valve bodies, bearing sleeves, wear rings and guide bushes |
| Production route | Drawing and alloy dependent; confirmed in quotation |
| Supply condition | Cleaned casting, rough-machined blank or finished component as ordered |
| Dimensions and weight | According to approved drawing; capability reviewed before acceptance |
| Casting tolerances | Agree relevant ISO 8062 tolerance and machining-allowance requirements |
| Machined tolerances | Feature-specific; no universal tolerance claimed |
| Surface finish | As-cast texture and machined roughness specified separately |
| Testing | Material, dimensional and functional checks according to the agreed inspection plan |
| Documentation | Specify certificate type, traceability and reports before order release |
Raw material grades
| Grade | Material description | Selection note |
|---|---|---|
| UNS C95400 | Copper-aluminum-iron bronze | Engineering wear components; confirm grade-specific requirements |
| UNS C95500 | Nickel aluminum bronze | Specify required properties and heat-treatment condition |
| UNS C95800 | Nickel aluminum bronze | Marine and pump applications subject to service review |
International equivalents and related designations
These references support alloy comparison. They are not blanket approvals to substitute material. Check the current standard edition, chemical limits, casting method, delivery condition and test requirements before accepting an alternative.
| Specified designation | International or related reference | Engineering qualification |
|---|---|---|
| C95400 | CuAl10Fe-type casting family | Related family only; compare exact chemistry and properties |
| C95800 | EN CC333G / CuAl10Fe5Ni5-C; legacy AB2 | Related nickel aluminum bronze family; chemistry limits differ, so not a direct substitute |
| C95500 | Nickel ab1 aluminum bronze casting specifications | No universal one-to-one substitute |
Product types and variants
| Variant | Typical procurement purpose | Drawing detail to define |
|---|---|---|
| As-cast component | Near-net blank for subsequent operations | Draft, fillets, gate dressing and casting tolerances |
| Rough-machined blank | Stock prepared for customer finishing | Reference datums and remaining allowance |
| Finish-machined component | Ready for inspection against finished drawing | Fits, threads, sealing faces and edge condition |
| Cored housing or body | Internal passage or hollow geometry | Core position and minimum final wall thickness |
| Ring, sleeve or bush | Rotational component considered for centrifugal casting | Bore stock, length, concentricity and material condition |
Applications in industry
Application selection for aluminum bronze should begin with wear resistance, mechanical loading and corrosion exposure. The component examples describe enquiry categories rather than a guaranteed rating or blanket suitability. The equipment designer remains responsible for the complete assembly, including loads, temperature, fluid compatibility and installation conditions.
| Customer group | Component or project context | Information needed |
|---|---|---|
| Electrical OEMs | Drawing-specific equipment bodies, supports or connection components | Electrical function, joint requirements and any conductivity requirement |
| EPC contractors | Plant equipment, pump and valve packages, maintenance spares | Project specification, service medium and inspection hold points |
| Power utilities | Auxiliary equipment, cooling systems and specified connection hardware | Duty conditions, traceability and equipment approval requirements |
| Industrial distributors | Repeat supply of identified casting components | Part number, drawing revision, alloy and stocking quantity |
Manufacturing process and casting methods
The production route is chosen after reviewing the material, geometry and order. The methods below are alternatives to assess; their inclusion does not mean every method is appropriate or available for every grade and part.
| Method | Suitable geometry or purpose | Important limitation |
|---|---|---|
| Sand casting | Complex housings, larger sections and flexible tooling | Surface texture, cores and allowances require review |
| Green sand casting | Repeat mold production using a moisture-containing sand system | Mold properties and gas control affect casting quality |
| Shell molding (resin sand) | Detailed smaller components using resin-coated sand shells | Tooling cost, core design and thermal behaviour must be assessed |
| Resin-bonded sand casting | Complex molds or cores with a chemically bonded sand system | Binder selection, gas evolution and reclamation differ from shell molding |
| Centrifugal casting | Rings, sleeves and rotationally symmetric blanks | Bore cleanup and machining allowance are required; not for arbitrary housings |
| Permanent mold casting | Repeat components where alloy and geometry suit reusable molds | Tooling, thermal control and core limitations require confirmation |
From drawing review to casting
The planned sequence begins with drawing review, alloy confirmation and process selection. Pattern or tool design establishes the parting arrangement, cores, draft and machining stock. Melt preparation and handling must preserve the required composition. Gating and feeding are planned around section changes and solidification behaviour. After pouring and cooling, the casting is removed from its mold, gates and risers are cut away, and the surface is cleaned. Each stage should support the agreed final acceptance criteria.
Secondary operations and release
Following cleaning, any specified treatment is completed in the agreed sequence. Rough machining can establish reference surfaces before critical features are finished. Inspection then checks dimensions, material identity and the functional tests required by the order. The supplier and purchaser should agree first-article approval before repeat production where the program requires it. Final release connects the accepted part to its documentation, marking and packaging. Changes to material, tooling, process or drawing revision should be reviewed before subsequent deliveries.
Quality standards and certification requirements
Specify the applicable standard and its edition in the purchase order. ASTM B584 addresses copper-alloy sand castings for general applications; ASTM B148 addresses aluminum-bronze sand castings; ASTM B271/B271M concerns copper-base centrifugal castings. EN 1982 provides a European framework for copper and copper-alloy ingots and castings. The selected standard must cover the actual alloy and product form.
Where requested, define the material inspection document, including any EN 10204 requirement, together with sampling and traceability. Dimensional inspection, chemical analysis, pressure testing and nondestructive examination are separate requirements. Request applicable current quality-system certificates and their scope during supplier qualification. This page does not claim that every casting is certified to every named standard, nor does a quality-system certificate replace product-specific acceptance evidence.
Why choose Brass Parts India
Use Brass Parts India as the enquiry point for a defined casting component rather than an unspecified metal shape. A useful technical quotation connects the alloy, drawing revision, production route, supply condition and inspection requirements. This makes it easier for purchasing and engineering teams to compare proposals on the same basis and identify exclusions before an order is placed.
For repeat supply, retain the approved first article, material specification and inspection plan as the purchasing reference. Discuss proposed substitutions or process changes before release. Request evidence for any capability, certification or special test that is essential to your project. Clear requirements and documented acceptance provide a more reliable basis for supplier selection than an unsupported general performance claim.
Frequently Asked Questions – AB1 Aluminum Bronze Casting
What is AB1 Aluminum Bronze Casting?
AB1 Aluminum Bronze Casting is a engineered metal casting used in industrial machinery, valves, pumps and OEM assemblies. Final suitability depends on the approved specification and application conditions.
Where is AB1 Aluminum Bronze Casting commonly used?
Typical applications include industrial machinery, valves, pumps and OEM assemblies. Confirm load, environment, mating parts and applicable standards before selection.
Which materials are available for AB1 Aluminum Bronze Casting?
Specify the specified brass, bronze, copper or aluminium-bronze grade. State the exact grade because similar commercial alloys can differ in composition and performance.
Which sizes can be supplied for AB1 Aluminum Bronze Casting?
Standard and custom sizes can be reviewed from casting drawing, machining allowance, wall section and critical dimensions. Nominal size alone may not define compatibility.
What dimensions are required to order AB1 Aluminum Bronze Casting?
Provide casting drawing, machining allowance, wall section and critical dimensions, with units, tolerances and drawing revision.
Can AB1 Aluminum Bronze Casting be made to a custom drawing?
Yes. Custom geometry, threads, tolerances and features can be assessed from a dimensioned drawing or approved sample.
Which thread standards are available for AB1 Aluminum Bronze Casting?
Relevant Metric, BSP, BSPT, NPT, NPTF, PG, BA or BSW threads may be considered. Specify form, size, pitch, class and engagement length.
Which finishes are offered for AB1 Aluminum Bronze Casting?
Options may include as-cast, machined, polished or coated. Specify coating type, thickness, appearance and corrosion or conductivity needs.
What tolerances can be maintained on AB1 Aluminum Bronze Casting?
Tolerance depends on material, size, geometry and process. Mark critical dimensions and fits clearly on the drawing.
How should AB1 Aluminum Bronze Casting be installed?
Check mating dimensions, orientation, sealing or retention method and specified tightening torque before use.
How is AB1 Aluminum Bronze Casting inspected?
Inspection can cover material identity, critical dimensions, threads, finish and drawing-specific functional checks.
Which quality documents are available for AB1 Aluminum Bronze Casting?
Material certificates, dimensional reports and coating or test records can be agreed at quotation stage.
Are samples available for AB1 Aluminum Bronze Casting?
Prototype or pre-production samples can be reviewed for new custom parts, subject to tooling and material requirements.
What are the MOQ and lead time for AB1 Aluminum Bronze Casting?
Minimum quantity and lead time vary with material, size, tooling, finish, inspection and order volume.
What is needed for a AB1 Aluminum Bronze Casting quotation?
Provide the drawing or specification, material, dimensions, tolerances, finish, quantity, inspection, packing and destination.