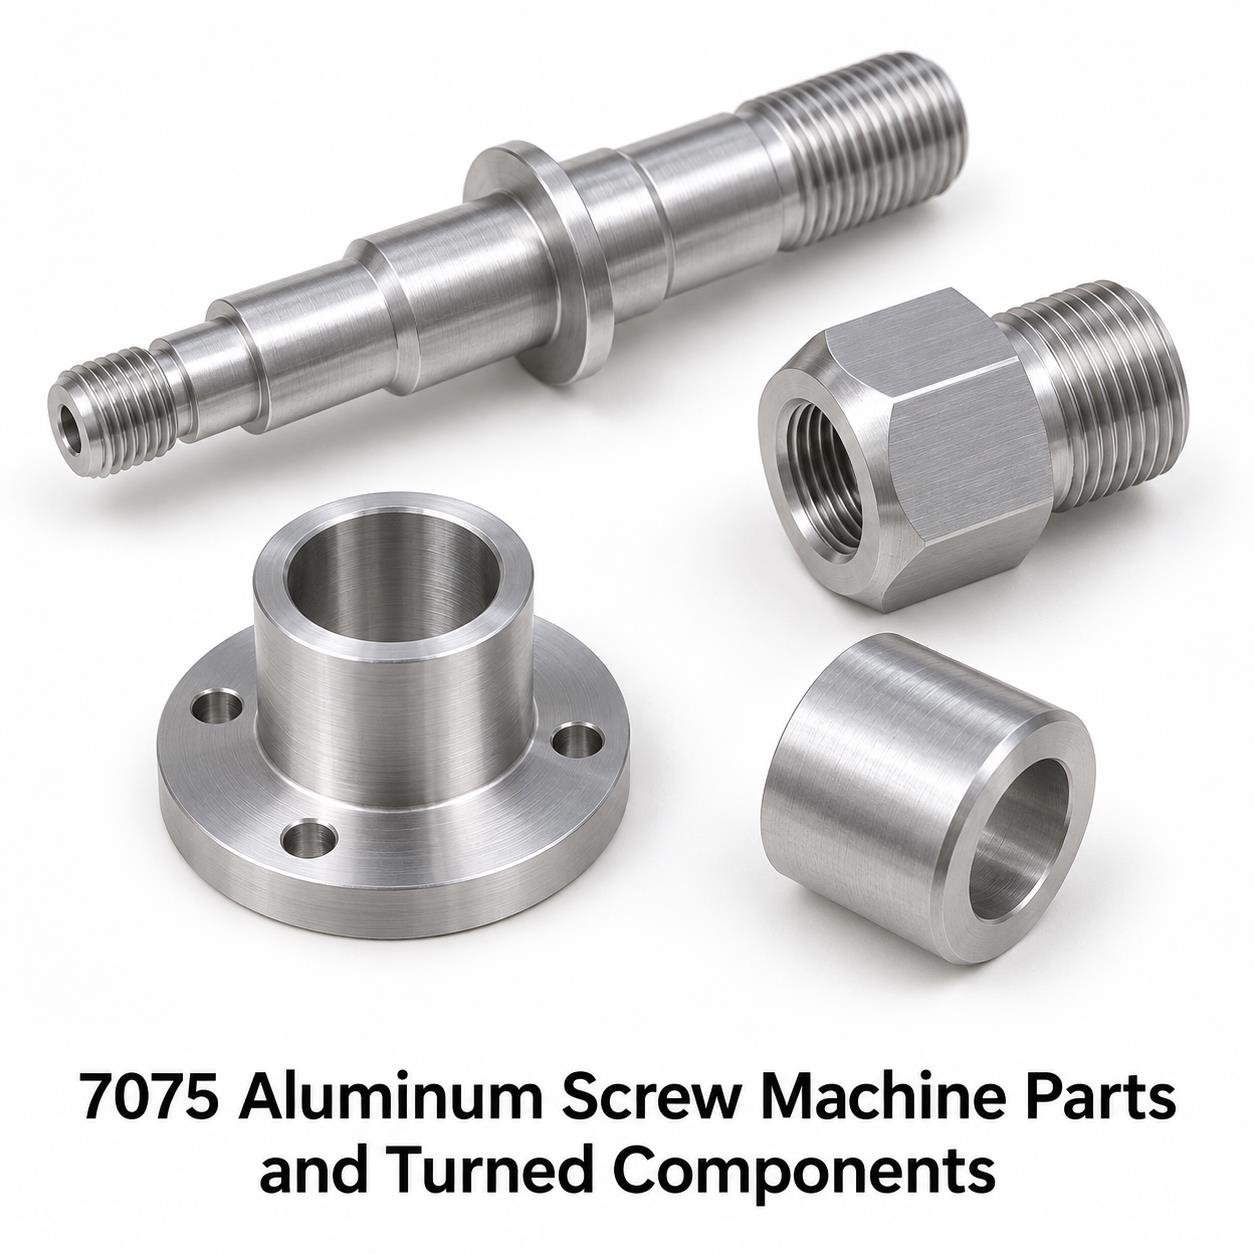
7075 Aluminum Screw Machine Parts and Turned Components
7075 aluminum screw machine parts and turned components are rotational, drawing-based parts produced from specified 7075 bar stock. CNC turning creates shoulders, bores, grooves and threads; secondary operations add wrench flats and cross holes. Brass Parts India accepts enquiries from electrical OEMs, EPC contractors, power utilities and distributors. Specify the exact temper because strength and resistance to stress-corrosion cracking differ between T6 and T73-family conditions. Typical parts include shouldered pins, threaded adapters, coupling hubs and precision spacers.
Price: US$ 12.00/Kg | Standard tolerance: ±0.05 mm
The final quotation confirms drawing complexity, quantity, chargeable weight, finishing, documentation and delivery terms.
Detailed product overview
Component geometry and functional interfaces
7075 Aluminum Screw Machine Parts and Turned Components cover component geometries such as shouldered pins, flanged bushes, threaded adapters, precision spacers, coupling hubs, retaining collars. Begin with the interface that controls assembly, then define supporting features from a consistent datum system. A shoulder can set axial position, a bore can locate a mating shaft, and a face can transfer clamping force. These functions require different checks. Include accessible tool reliefs and avoid unspecified sharp internal corners. Identify which dimensions must remain correct after finishing and which are reference values. The approved drawing should connect each acceptance requirement to the intended mechanical function.
Material selection and service conditions
7075 is a heat-treatable aluminum-zinc-magnesium-copper alloy used where mechanical strength is a principal selection criterion. T6 and T651 conditions differ from overaged T73 and T7351 conditions; the latter trade some strength for improved resistance to stress-corrosion cracking. The specified stock form and dimensions govern applicable mechanical requirements. Do not select a temper from an alloy name alone. For sustained loads or corrosive exposure, define the service conditions and review grain orientation, protective finish and mating materials before approving the component specification.
Datums, dimensions and repeatable assembly
The standard tolerance for these parts is ±0.05 mm. Define the reference face, axis or datum system used to inspect the component. Position, perpendicularity, coaxial features and surface texture need their own drawing requirements when they influence assembly. A nominal dimension without its tolerance can lead to different interpretations during machining and inspection. Provide limits for critical interfaces, and distinguish functional dimensions from reference information. For flanged bushes, identify the features that control location rather than applying unnecessarily restrictive requirements everywhere.
Machining behaviour and part support
7075 screw machining requires a route matched to the bar diameter, unsupported length and feature sequence. Establish a sound reference face before finishing shoulders and bearing seats. Thin threaded walls and deep grooves can reduce the effective section significantly, even in a high-strength alloy. Provide root radii and relief dimensions where loading makes them important. Chips and burrs must be removed from cross holes without damaging finished bores. Conventional fusion welding is generally unsuitable for this alloy; assembly design should identify the intended mechanical joining method.
Surface condition and assembly preparation
Available finish routes are specified as machined aluminum, anodizing or another specified protective finish. The drawing should define whether a surface is functional, cosmetic or both. Break sharp edges in accordance with the agreed requirement while protecting contact faces, thread starts and sealing lands. Cleaning needs depend on the service: residual chips, machining fluid or polishing compound can affect assembly. For coupling hubs, identify surfaces that must remain free from coating or mechanical damage. Confirm whether dimensional acceptance is required before finishing, after finishing or at both stages.
Purchasing information and production scope
Procurement teams should describe retaining collars by a controlled part number rather than by a photograph alone. A complete enquiry includes the drawing revision, quantity, material designation, finish and destination. State whether the order is a prototype, scheduled release or repeat requirement. The listed kilogram rate provides a commercial reference, but the written quotation must define its scope and weight basis. Keeping technical and commercial information together helps electrical OEMs, EPC contractors, utilities and distributors compare offers on the same requirements.
Key features
- Drawing-based CNC bar turning with secondary milling and drilling
- Standard dimensional tolerance ±0.05 mm; individual requirements subject to drawing review
- aluminum grade and condition specified before production
- Turned, bored, drilled, threaded or milled features according to geometry
- Finish and edge requirements linked to component function
- Inspection and material documentation agreed with the purchase order
Bores, holes and internal features
For aluminum components, specify through holes and blind holes separately, including usable depth and any drill-point allowance. Identify cross holes that intersect a bore so the deburring approach can be considered. A dimensioned bore may serve as clearance, location, bearing support or a flow passage; these functions can require different finish and inspection methods. Provide the mating diameter or fit requirement where relevant. Do not infer a sealing or pressure capability from an internal passage alone.
Threads and fastening interfaces
Define thread system, nominal size, pitch, internal or external form, engagement length and acceptance class. Metric, unified and pipe threads are different specifications and should not be mixed under a generic threaded-parts description. Include the required gauge basis and any post-plating allowance. For threaded adapters, check wall thickness around the thread and provide adequate entry chamfers. Torque, locking method and service loading belong to the assembly specification and should be supplied when they affect the component design.
Grooves, slots and tool clearance
Grooves and slots should show width, depth, root radius and position from an identified datum. A sharp internal corner shown in a model may require an alternative radius or a different operation. State whether a groove locates a retaining element, provides clearance or carries a seal. The required edge condition should preserve the intended function. With CNC bar turning with secondary milling and drilling, access and component support influence the sequence; review narrow features and deep recesses before fixing the final drawing.
Contact faces and mating surfaces
Describe the actual function of each mating face. Mechanical seating, electrical contact and sealing do not necessarily require the same preparation. Specify flatness or roughness where the assembly needs it instead of treating the general ±0.05 mm dimensional tolerance as a surface specification. For shouldered pins, identify contact zones, prohibited coating areas and acceptable handling marks. The equipment designer remains responsible for validating the complete joint under operating loads, temperature and environmental conditions.
Inspection planning and traceability
Inspection should follow the drawing’s critical features and the agreed sampling plan. Suitable measurement methods depend on feature size, accessibility and tolerance; the presence of a CNC machine is not an inspection record. Specify whether a first-article report, dimensional layout, material certificate or batch identification is needed. Maintain a clear connection between the drawing revision and ordered aluminum grade. Special documentation and retained samples should be requested before production so the commercial offer includes the required work.
Packaging and repeat-order control
Protect finished threads, bores and contact faces during handling and transport. Separate components where metal-to-metal movement could damage a functional surface. Specify part-number labels, batch information and package quantities when they are needed for stores control or assembly lines. Repeat orders should refer to the approved drawing revision and any accepted deviations. If retaining collars are supplied with other components, identify each item independently to avoid mixing similar-looking materials or variants during receipt and installation.
Technical specifications
| Parameter | Specification / ordering information |
|---|---|
| Product | 7075 Aluminum Screw Machine Parts and Turned Components |
| Brand | Brass Parts India |
| Manufacturing route | CNC bar turning with secondary milling and drilling |
| Standard dimensional tolerance | ±0.05 mm |
| Raw material | 7075; T6, T651; T73 or T7351 subject to form and design |
| Dimensions and geometry | Customer drawing; confirm feasibility before order |
| Thread specification | Drawing-defined system, size, pitch, class and engagement |
| Surface treatment | machined aluminum, anodizing or another specified protective finish |
| Surface roughness and geometric controls | Individually specified where required; not implied by general tolerance |
| Inspection and documents | Agreed inspection plan, material records and reporting scope |
| Listed rate | US$ 12.00/Kg; written quotation defines scope |
| Order information | Part number, revision, quantity, finish, documentation and destination |
Raw material grades and international references
EN AW-7075; AlZn5.5MgCu. The following international designations identify alloy families; they do not establish unconditional equivalence of delivered stock. Match composition, temper, product form, mechanical limits and inspection documents. Different rows are alternative materials requiring design approval.
| Alloy | European numerical designation | Chemical designation | Condition to specify |
|---|---|---|---|
| 6061 | EN AW-6061 | AlMg1SiCu | T6 / form-specific stress-relieved condition |
| 7075 | EN AW-7075 | AlZn5.5MgCu | T6 / T73 families; confirm exact temper |
| 2024 | EN AW-2024 | AlCu4Mg1 | T4 / T351 or drawing-approved temper |
| 5083 | EN AW-5083 | AlMg4.5Mn0.7 | O / H111; H116/H321 for specified plate |
| Product form / requirement | Specification framework to confirm |
|---|---|
| Extruded rod, bar or shapes | ASTM B221 or applicable EN 755 product requirements |
| Rolled plate or sheet | ASTM B209 or applicable EN 485 product requirements |
| Cold-finished stock | Applicable product specification and dimensional limits |
| Material inspection document | EN 10204 document type if ordered and available |
Product types and variants
| Variant | Features to define |
|---|---|
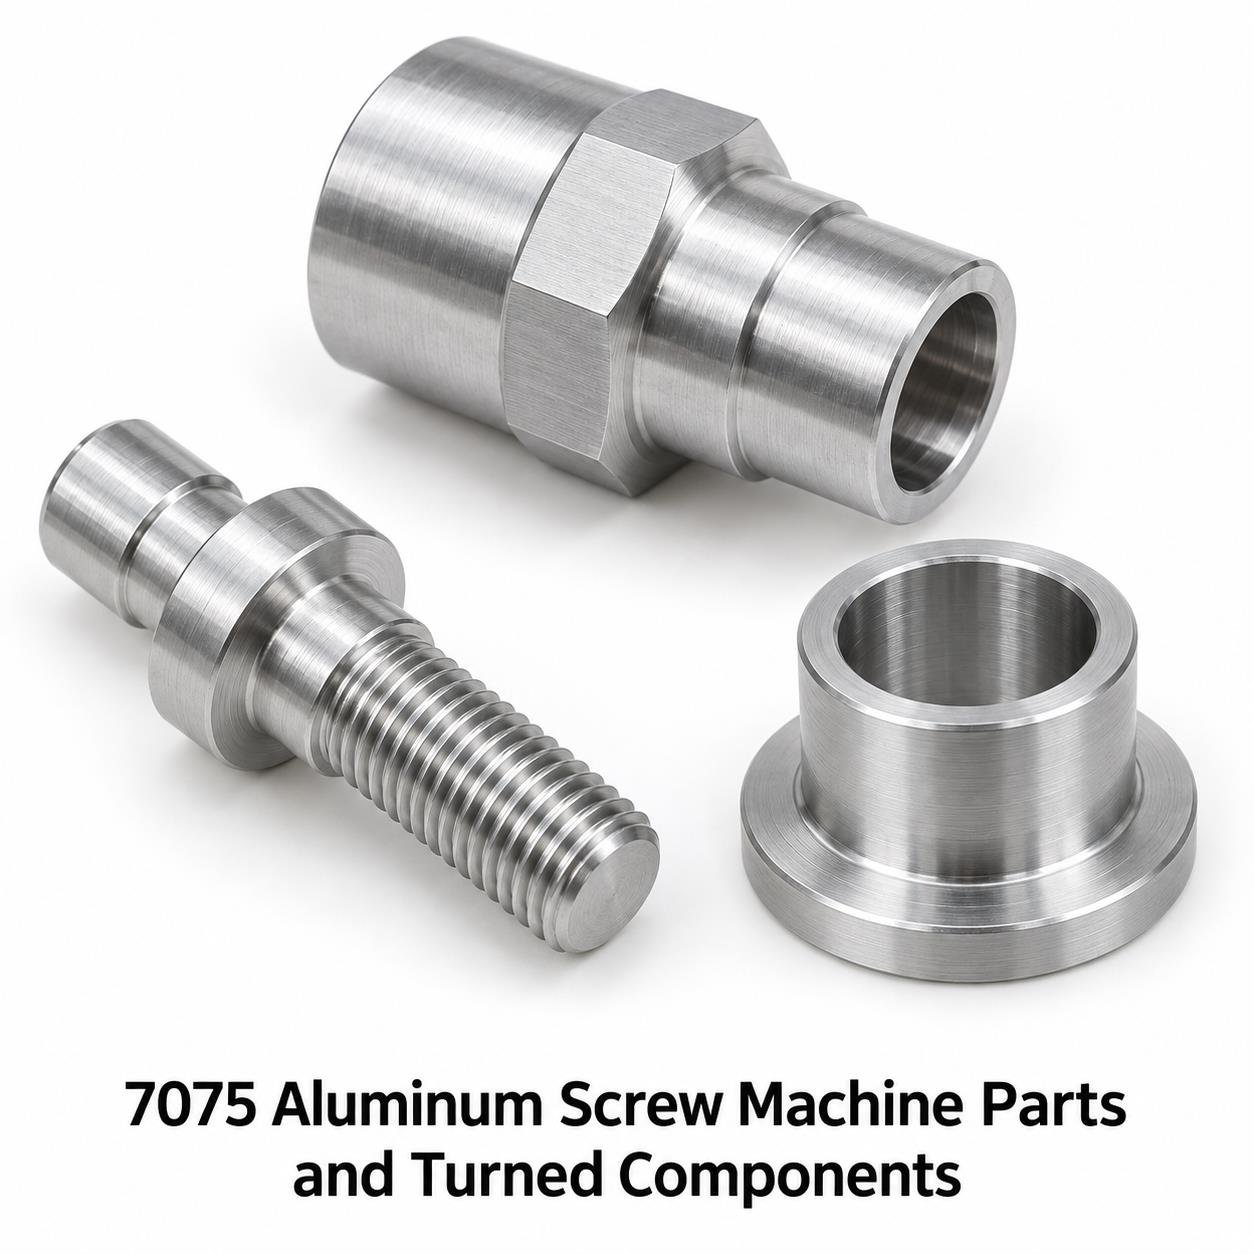
| shouldered pins | Overall length, steps and functional datums |
| flanged bushes | Mating diameters, shoulders and surface condition |
| threaded adapters | Thread details, engagement and entry geometry |
| precision spacers | Bore limits, wall thickness and edge breaks |
| coupling hubs | Ports, flats, mounting holes and contact zones |
| retaining collars | Thickness, location and handling requirements |
Industrial applications
| Customer / sector | Potential component role | Information needed |
|---|---|---|
| Electrical OEMs | Connector, terminal, enclosure or mounting interfaces | Electrical function, mating geometry, finish and assembly validation |
| EPC contractors | Project-specific equipment and installation components | Approved drawings, schedules and project documentation |
| Power utilities | Equipment maintenance and replacement components | Original specification, operating conditions and approval route |
| Distributors | Repeat supply of identified drawing-based parts | Part numbers, revisions, quantities and packaging |
| Instrumentation and industrial equipment | Spacers, housings, adapters and mechanical interfaces | Loads, environmental exposure and functional tolerances |
Application suitability depends on the complete design. An alloy number without a temper is an incomplete mechanical specification. Anodizing changes surface dimensions and electrical contact behaviour; coating thickness, masking and final inspection dimensions must be agreed before machining. Provide temperature range, exposure conditions and expected mechanical or electrical function when these affect material choice. Equipment ratings, pressure limits and compliance claims require assembly-level evidence. The component drawing should capture the features needed to support that validation rather than relying on a generic catalogue description.
Manufacturing process
1. Drawing and material review
Review the aluminum grade, dimensions, datum structure and finish together. Identify features that need additional clarification, such as inaccessible burrs, incomplete thread callouts or conflicting limits. Confirm the controlled revision and obtain approval for any proposed change before manufacture.
2. Stock preparation and setup
Select the specified stock form and condition, then plan cutting allowances and workholding. Thin aluminum sections can distort under clamping. Tool geometry, chip clearance, residual stress and the chosen temper affect the final fit and surface quality. The setup should provide access to required features while protecting surfaces that are already finished.
3. Controlled machining sequence
CNC bar turning with secondary milling and drilling creates the principal geometry. Roughing removes excess material before the relevant finishing operations establish drawing features. Drilling, boring, tapping, slotting or secondary milling are added where required. Tool selection and cutting conditions depend on the actual alloy and geometry.
4. Edge finishing and cleaning
Remove burrs to the agreed edge specification, especially at intersecting holes and thread starts. Avoid rounding a functional edge beyond the drawing allowance. Clean the components using a method compatible with the material and subsequent finishing or assembly requirements.
5. Surface treatment and verification
Apply machined aluminum, anodizing or another specified protective finish only as ordered. Check the effect on fit and functional surfaces, including masked areas. Verify the required dimensions in the agreed finished condition and review the specified inspection records before release.
6. Identification and dispatch
Identify parts and packages against the order and drawing revision. Protect functional surfaces for the selected transport route. Include the agreed documentation and distinguish separate batches or materials where the purchase order requires traceability.
Quality standards and certification requirements
Quality requirements must be tied to the supplied part and order. Ask for the current applicable ISO 9001 certificate if supplier quality-system certification is required; confirm its scope and validity. Certification scope and validity must be checked for the supplying facility and ordered work. Material records, including an EN 10204 document where specified and available, should match the supplied grade and batch. A material certificate does not replace dimensional inspection or finished-equipment approval.
| Requirement | How to specify it |
|---|---|
| Material conformity | Exact grade, standard, condition and certificate type |
| Dimensional acceptance | Drawing revision, critical features and inspection plan |
| Restricted substances | Applicable jurisdiction, permitted limits and evidence required |
| Finish verification | Coating type, thickness, masking and acceptance method |
| Application approval | Relevant assembly or project standard and responsible approval authority |
Why choose Brass Parts India for this enquiry?
A useful quotation starts with an engineering definition of the aluminum part. Brass Parts India receives drawing-based enquiries in this CNC and VMC category from its Jamnagar, India contact location. Domestic and international purchasing teams can specify destination, packing and documentation within the same enquiry. Compare offers using the same grade, tolerance, finish and documentation scope. The supplied rate is visible here so purchasing teams can begin a commercial discussion with a clear reference, while the approved drawing remains the basis of manufacture.
Related parts and internal product links
Aluminum CNC Turned Parts parent range
- 6061 Aluminum Machined Parts
- 2024 Aluminum Machined Parts, CNC Machined Components
- 5083 Aluminium Alloy Machined Parts
- Aluminum VMC Milled Parts in All Alloys
- Swiss Machining of Brass and Brass Sliding head Components and Parts
- Stainless Steel 316 CNC machined Parts
- Brass Lead Free CNC Machined Components
- Free Cutting Brass CNC machined Parts
- Copper CNC machined Components
- Copper VMC milled Components and Parts
Explore the CNC and VMC machined parts category. Compare processes and materials against the component function; related pages are alternatives for discussion, not automatic substitutes.
Equivalent product terms in other languages
Use these purchasing terms with the alloy designation and approved drawing. Translated names do not change material or inspection requirements.
| Language | Related technical terms |
|---|---|
| Spanish | piezas mecanizadas de aluminio 7075; componentes de aluminio CNC; fresado de aluminio |
| Russian | детали из алюминия 7075; обработка алюминия на ЧПУ; фрезерованные алюминиевые детали |
| French | pièces usinées en aluminium 7075; composants aluminium CNC; fraisage aluminium |
| Portuguese | peças usinadas de alumínio 7075; componentes de alumínio CNC; fresagem de alumínio |
| Italian | parti lavorate in alluminio 7075; componenti in alluminio CNC; fresatura alluminio |
Request a technical quotation
Send the drawing and revision, aluminum grade, order quantity, finish, inspection requirements and delivery destination to Brass Parts India. Quote this product title and the listed US$ 12.00/Kg rate. Identify any individual tolerance differing from the standard ±0.05 mm. Request confirmation of price scope, material availability, production schedule and shipping terms in the written offer.
Contact us about your machined components.
Frequently asked questions
What tolerance is offered?
The standard dimensional tolerance is ±0.05 mm. Individually toleranced dimensions, geometric controls, threads and surface finish must be agreed from the drawing. This value is not a blanket flatness, runout or roughness specification. State whether acceptance applies before or after finishing.
What is the price per kilogram?
The listed rate is US$ 12.00/Kg. Request a written quotation for your drawing, material grade, quantity and delivery destination. Confirm the chargeable weight basis, machining scope, finishing, inspection, packing, taxes and freight before ordering.
Should I specify 7075-T6 or a T73-family temper?
Choose from the design requirements. T6-family conditions emphasize high strength; T73-family conditions improve stress-corrosion resistance with a strength tradeoff. Stock form, section thickness, grain direction and environment affect acceptance. The drawing and purchase order must state the exact approved temper.
Can parts be made to a customer drawing?
Send a dimensioned drawing with revision, a STEP model where available, and the required quantity. Include the functional datums, mating interfaces, thread details and critical dimensions. CNC bar turning with secondary milling and drilling and secondary operations can then be reviewed against the complete specification.
Are the catalogue images exact stock items?
The images are representative product illustrations. They show typical part forms, not proof of a particular alloy, dimensional capability or stock availability. The approved drawing and order specification determine the supplied geometry, material, finish and acceptance requirements.
Which finishes can be requested?
Finish options include machined aluminum, anodizing or another specified protective finish. State the coating system, thickness, appearance and masking requirements where applicable. Finishing can change fit, conductivity and corrosion behaviour; critical dimensions should identify the required finished condition.
Are certifications included automatically?
Certification must be agreed in the purchase order. Request the applicable current quality-system certificate, material test documentation and inspection records before placing the order. A raw material designation or general manufacturing description does not establish approval for a regulated finished assembly.
What should an OEM or EPC quotation request include?
Include drawing number and revision, material grade, order quantity, expected repeat demand, inspection plan and destination. Identify traceability, finish, packing and project documentation requirements. For electrical or pressure-related service, supply the assembly conditions and applicable approval requirements.
Can these parts be used in electrical equipment?
Potential applications depend on the function assigned to the aluminum component. Review electrical contact behaviour, mechanical loading, temperature, corrosion exposure and insulation clearance at assembly level. A machined part alone does not establish the current, voltage, ingress-protection or short-circuit rating of equipment.
How are related components ordered together?
List each part number and drawing revision separately, even when several items use the same material. Provide quantities and inspection requirements per line. Related CNC and VMC products are linked above so procurement teams can group enquiries while keeping each technical specification distinct.