Transformer Spade Terminals, Transformer Spade Connectors
Brand: Cable Glands India | Price: US$ 18/kg
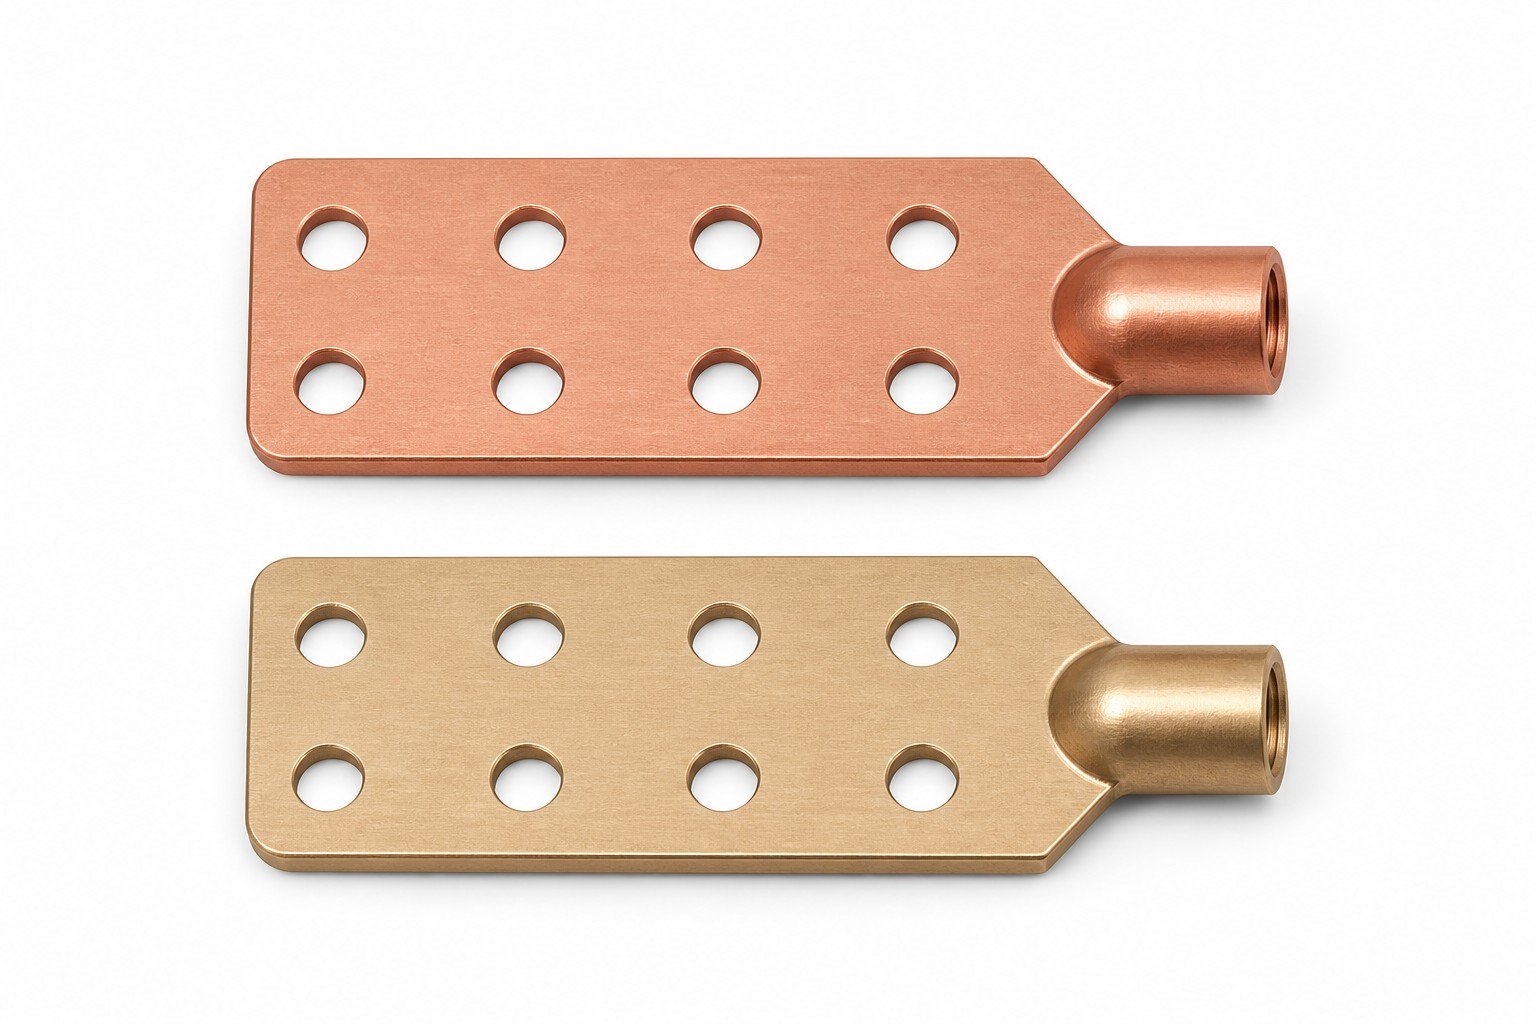
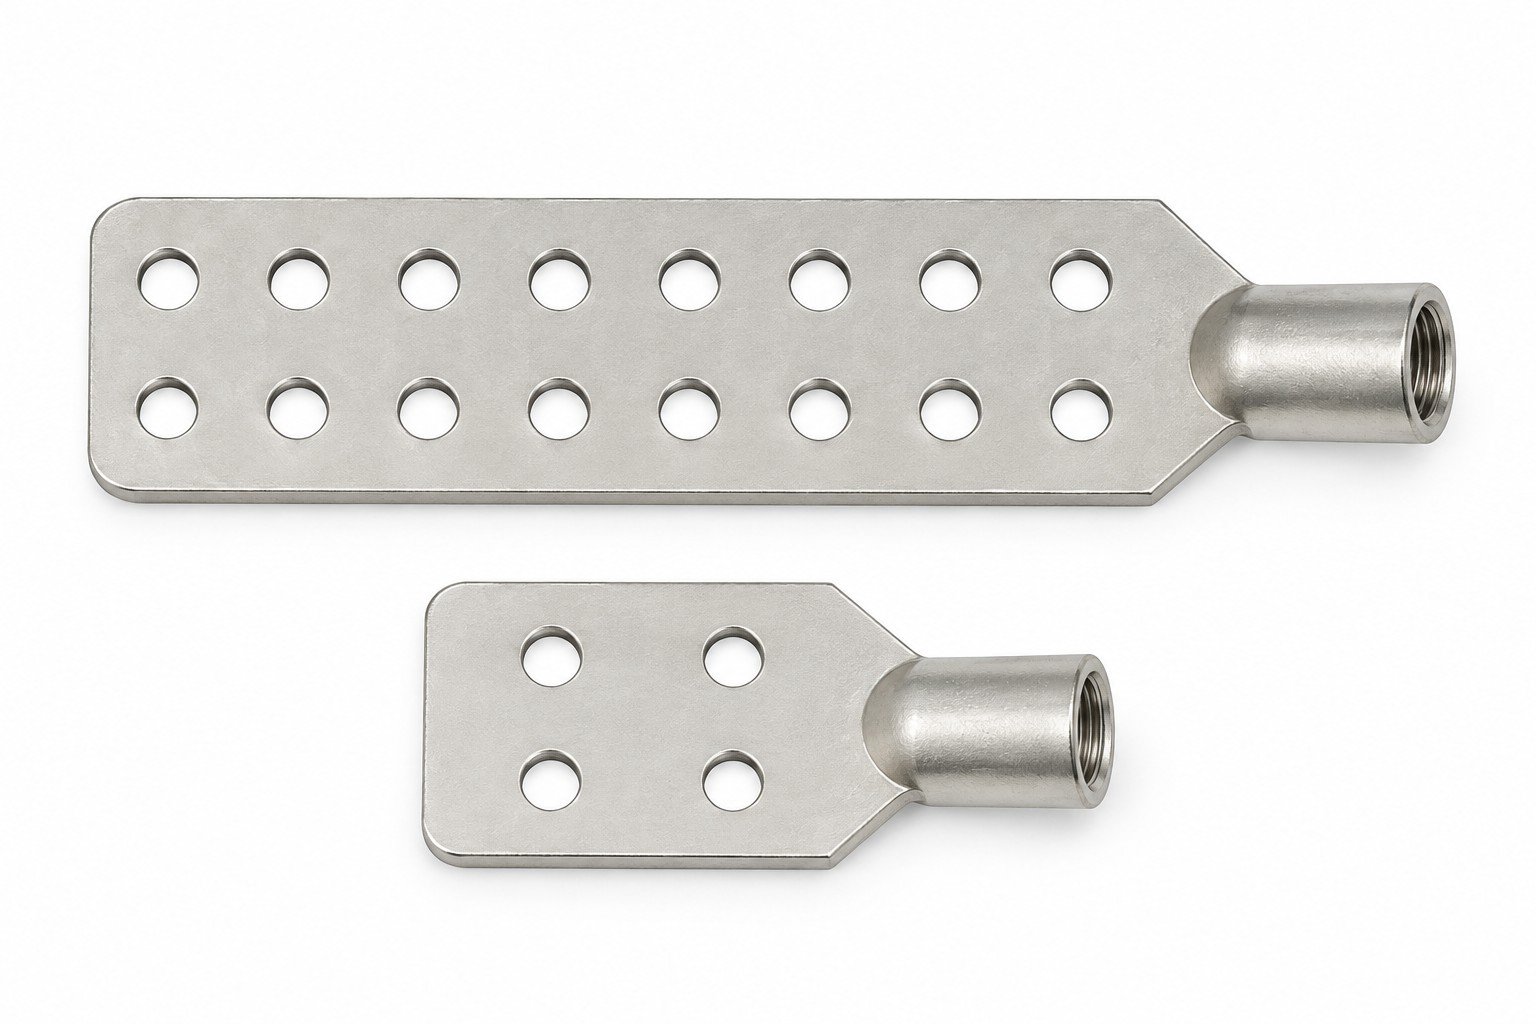
Cable Glands India transformer spade terminals connect a transformer bushing stud to a flat, bolted cable-lug or busbar interface. The straight inline design follows the transformer stud axis into the connection palm. This range covers NEMA-spaced configurations from 2 to 16 holes, bronze and copper alloys including CDA 833, CDA 836, CDA 844 and Copper C110, and natural or tin-plated finishes. Nominal thread diameters are 3/8 inch, 1/2 inch, 3/4 inch and 1 inch, with UNC, UNF, UNEF or UNS specifications selected to match the approved drawing.
Designed for electrical OEM procurement, EPC projects, utility maintenance and distributor sourcing, each terminal must be selected against its mating stud, palm geometry, conductor arrangement and electrical duty. Submit your drawing for a configuration-specific quotation.
Transformer Spade Connector Product Overview
Transformer Bushing Stud Connections
A transformer spade connector provides a mechanical and electrical transition between a bushing terminal and outgoing conductors. Its threaded hub engages the specified transformer stud, while the flat palm supports bolted connections. Stud diameter alone does not establish compatibility. Pitch, engagement length, thread class and available clearance also matter. The terminal must seat without bottoming prematurely or imposing unintended loads on the bushing. Assembly access should accommodate the approved tooling and hardware. Include the bushing drawing when requesting a replacement. This helps coordinate the complete connection rather than treating the terminal as an isolated metal component.
NEMA-Spaced Terminal Palms
The palm is the flat connection surface carrying the bolt-hole pattern. NEMA-spaced arrangements help coordinate mating cable lugs, busbar pads and terminal accessories. Specify actual centre distances, hole diameter, row layout and edge distances on the drawing. A shared hole pattern does not establish current capacity or universal interchangeability. Palm thickness and usable contact area also affect joint design. Bolt heads, washers and lug barrels need sufficient clearance. For multirow configurations, check access to every fixing position. The final pattern must match both the mating component and the equipment envelope.
Two-Hole to Sixteen-Hole Configurations
The range extends from compact two-hole terminals to larger sixteen-hole arrangements. Intermediate combinations support different equipment layouts and connection requirements. The number of holes describes the palm pattern, not the number of independent electrical circuits. Multiple conductors attached to one terminal remain part of the same connected node. Lug positions must account for cable bend radius and mechanical support. Larger palms can increase the lever arm acting on a transformer stud. Therefore, confirm bracing and installation space before increasing terminal size. Hole combinations, overall dimensions and permitted loading are drawing-specific.
Bronze and Copper Alloy Selection
CDA 833, CDA 836 and CDA 844 are familiar purchasing names for cast copper-base alloys. Their formal UNS designations are C83300, C83600 and C84400. They are frequently described commercially as bronze, although their metallurgical classifications include red and semi-red brasses. Copper C110 corresponds to wrought C11000 electrolytic tough-pitch copper. These materials differ in composition, conductivity, strength and manufacturing behaviour. They should not be substituted solely because their colour or dimensions appear similar. State the full alloy designation and required product form. Confirm any proposed alternative against the equipment specification.
Natural and Tin-Plated Contact Surfaces
Natural finish leaves the selected copper alloy unplated after the agreed cleaning and machining operations. Tin plating introduces a specified metallic coating over the prepared substrate. Finish selection should consider the mating material, environment and maintenance practice. Coating thickness, adhesion and coverage belong in the purchasing specification. Threads may require allowance or masking according to the approved design. Tin plating does not establish aluminium-conductor compatibility by itself. Contact preparation and bolting practice remain essential. Both finishes require protected handling to avoid damage to critical mating faces.
OEM Drawings and Replacement Requirements
A controlled drawing provides the common reference for manufacture, inspection and installation. Include the terminal orientation, hub position and any offset between the stud axis and connection palm. Identify critical datums and tolerances instead of relying on overall dimensions alone. Replacement parts also require confirmation of the existing bushing condition and stud specification. Sample measurements can support development, but worn components may not represent original tolerances. Define the required material and finish before sample approval. Record the drawing revision on the purchase order. This supports consistent repeat ordering and clear acceptance criteria.
Key Features
- NEMA-spaced transformer connection palms in 2–16-hole combinations.
- CDA 833, CDA 836, CDA 844 and C110 copper material options.
- Natural metal or tin-plated finish.
- 3/8-inch, 1/2-inch, 3/4-inch and 1-inch nominal threads.
- UNC, UNF, UNEF and UNS thread specifications to approved drawings.
- Configurable palm, hub and connection geometry.
- Drawing-based selection for OEMs, EPC contractors, utilities and distributors.
Electrical Contact Faces
Flat mating surfaces support controlled contact between the terminal and the attached lug or busbar. Surface condition should be assessed before assembly. Burrs, distortion and contamination can prevent the intended seating. Specify flatness and surface finish where they affect the joint. The installation design must establish contact pressure and fastening arrangements. A visually polished surface alone does not demonstrate electrical performance. Where required, evaluate contact resistance and temperature rise on the representative assembled connection.
Unified Thread Engagement
UNC, UNF, UNEF and UNS describe distinct Unified thread specifications. A complete callout includes nominal diameter, threads per inch and tolerance class. Internal and external thread classes must be identified correctly. Engagement length should be compatible with the stud and connector material. Specify whether the thread is through or blind. Include any relief, counterbore or seating requirement. Check the finished thread after coating when plating affects fit. Do not force a connector onto a partially matching stud.
Busbar and Cable Lug Integration
Transformer terminal palms can interface with compatible bolted lugs and busbar connections. Matching bolt centres is only one part of this assessment. The lug palm must fit within the available contact surface. Fastener length must suit the complete joint stack. Cable routing should prevent excessive bending loads on the terminal. Busbar supports should address vibration and thermal movement. Aluminium connections require a specifically approved joint system. Confirm conductor material, lug details and installation instructions together.
Material Traceability
Material identification starts with the full grade and applicable purchasing specification. A traceability plan should connect incoming material or casting heat to the finished batch. Chemical analysis is relevant when similar-looking alloys have different compositions. Inspection records should reference the order and drawing revision. Agree identification methods that do not damage contact faces. Define whether individual or batch marking is needed. The quotation should identify the documentation included and any additional testing requested by the purchaser.
Finish and Corrosion Considerations
Natural and tin-plated terminals need service-specific evaluation for humidity, contamination and dissimilar-metal contact. Tin coating can provide a controlled contact surface, but coating defects and exposed edges require consideration. Specify the plating system rather than requesting only a colour. Packaging should prevent abrasion during transport. Installation preparation must follow the equipment manufacturer’s instructions. Avoid assuming that a plated terminal is suitable for every outdoor environment. Environmental qualification should reflect the complete connector assembly and intended service.
Mechanical Fit and Service Access
Terminal geometry affects assembly access as well as electrical layout. Check spanner clearance around the hub and tool access around palm bolts. Confirm that adjacent phases, barriers and enclosure surfaces remain clear. The equipment designer must establish the necessary electrical clearances. Larger hole patterns require particular attention to support and cantilever loading. Include any space restrictions with the enquiry. Clear dimensional requirements help reduce installation rework and support repeatable fit across production batches.
Technical Specifications
| Parameter | Specification / selection requirement |
|---|---|
| Product category | Electrical Accessories; transformer spade terminals and connectors |
| Brand | Cable Glands India |
| Palm configuration | 2–16 holes; NEMA-spaced arrangement to approved drawing |
| Materials | UNS C83300, C83600, C84400; wrought C11000 copper |
| Finish | Natural or tin-plated; coating requirements to order |
| Nominal thread diameters | 3/8 inch, 1/2 inch, 3/4 inch, 1 inch |
| Thread series | UNC, UNF, UNEF, UNS; exact pitch and class to drawing |
| Dimensions and tolerances | Palm width, thickness, hole centres, hub and thread engagement as specified |
| Electrical duty | Current, temperature rise and short-circuit requirements need assembly-specific validation |
| Installation torque | Defined by the approved connector, stud and hardware arrangement |
| Price basis | US$ 18/kg; confirm configuration, order mass and commercial terms in quotation |
Raw Material Grades and Principal Composition
| Purchasing grade | UNS | Principal composition, mass % | Material form |
|---|---|---|---|
| CDA 833 | C83300 | Cu 92–94; Sn 1–2; Pb 1–2; Zn 2–6 | Cast copper alloy |
| CDA 836 | C83600 | Cu 84–86; Sn 4–6; Pb 4–6; Zn 4–6 | Cast leaded red brass / ounce metal |
| CDA 844 | C84400 | Cu 78–82; Sn 2.3–3.5; Pb 6–8; Zn 7–10 | Cast leaded semi-red brass |
| Copper C110 | C11000 | Cu including Ag: 99.90 minimum | Wrought electrolytic tough-pitch copper |
These principal-element ranges are identification guidance, not a complete acceptance specification. Apply all impurity limits, composition notes, product-form requirements and test conditions in the ordered material standard. C11000 is not a cast bronze grade. Material properties must correspond to the actual form and condition supplied.
International Designation and Equivalent-Material Guide
| US designation | International / commercial reference | Equivalence status |
|---|---|---|
| CDA 833 / UNS C83300 | Copper-tin-zinc-lead cast alloy | No blanket EN, DIN, BS or JIS substitute specified; compare full requirements |
| CDA 836 / UNS C83600 | Ounce metal; nominal 85-5-5-5 composition | Commercial description, not automatic international interchangeability |
| CDA 844 / UNS C84400 | Leaded semi-red brass / valve metal | Approve any alternative through chemistry and product-form comparison |
| UNS C11000 | EN CW004A / Cu-ETP | Common counterpart; verify temper, dimensions and applicable product standard |
For international tenders, submit the proposed local grade and its specification. Similar nominal chemistry does not guarantee equivalent conductivity, mechanical properties or inspection requirements. Written substitution approval should precede production.
Product Types and Variants
| Variant | Typical selection purpose | Required confirmation |
|---|---|---|
| 2-hole spade terminal | Compact bolted connection | Lug footprint and stud compatibility |
| 4-hole spade connector | Wider connection palm | Row spacing and hardware clearance |
| 6–8-hole configuration | Extended connection arrangement | Palm support and cable routing |
| 10–16-hole configuration | Larger multi-position palm | Mechanical loading and available equipment space |
| Natural bronze or copper | Specified unplated interface | Material grade and surface preparation |
| Tin-plated connector | Specified coated interface | Coating thickness, coverage and finished thread fit |
Listed combinations define the product range; individual dimensions and production availability are confirmed against the enquiry. Odd-hole or asymmetric arrangements require explicit drawing review.
Industrial Applications
| Customer / industry | Potential application | Engineering check |
|---|---|---|
| Transformer OEMs | Bushing-stud to cable-lug transitions | Stud fit and validated electrical duty |
| EPC contractors | Transformer connections in power projects | Approved equipment interface drawings |
| Power utilities | Replacement terminal assemblies | Existing bushing and conductor compatibility |
| Industrial plants | Transformer-fed distribution equipment | Clearance, enclosure and maintenance access |
| Renewable-energy projects | Project-specific transformer terminations | Duty cycle, environment and joint qualification |
| Electrical distributors | Drawing-matched supply programmes | Variant identification and documentation |
Manufacturing Process and Inspection Planning
The manufacturing route depends on the alloy, geometry and order requirements. Cast-alloy connectors and wrought-copper parts need different starting forms. The following sequence provides a basis for agreeing the production and inspection plan; the quotation should confirm the operations and records included.
- Drawing review: establish material, palm pattern, thread callout, datums and acceptance criteria.
- Material preparation: select the specified casting or wrought stock route and identify the material batch.
- Blank production: produce a suitable casting or prepare a wrought blank with machining allowances.
- Machining: finish contact faces, hub features and hole locations to the approved dimensions.
- Thread cutting: machine the specified thread and verify engagement and fit using the agreed gauges.
- Finishing: deburr, clean and apply tin plating where ordered; protect critical surfaces.
- Final inspection: verify dimensions, finish and identification against the inspection plan before packing.
Quality Standards and Certification Requirements
| Reference / document | Relevant scope | Purchasing approach |
|---|---|---|
| ASME B1.1 | Unified inch screw threads | Specify applicable edition, pitch and class |
| ASTM B584 | Copper-alloy sand castings | Use where the selected alloy and casting route are covered |
| ASTM B62 | Composition bronze / ounce-metal castings | Consider for applicable C83600 castings |
| ASTM B545 | Electrodeposited tin coatings | Specify coating class and required inspection |
| Material and dimensional reports | Order-specific conformity evidence | Agree traceability and report scope before ordering |
| ISO, UL or other certificates | Organisation or product-specific certification | Request current documents and verify their scope |
Listing a reference standard does not claim that every variant is certified to it. NEMA-spaced geometry does not constitute NEMA product certification. No universal current rating, UL listing or company certification is asserted for this range. Specify any qualification testing and compliance documents required by your project.
Why Choose Cable Glands India for This Product?
This range brings multiple palm configurations, four stated material options and two finish choices into one drawing-based enquiry. Buyers can define the connector around the required bushing interface rather than selecting only by a generic product name. The published US$ 18/kg rate gives a clear starting point for commercial discussion. Compare quotations using the same alloy, finished weight, coating and inspection scope. For repeat procurement, retain the approved drawing, sample acceptance record and configuration description with the purchase order.
Frequently Asked Questions – Transformer Spade Terminals, Transformer Spade Connectors
What is Transformer Spade Terminals, Transformer Spade Connectors?
Transformer Spade Terminals, Transformer Spade Connectors is a electrical connection component used in power distribution, grounding and cable termination. Final suitability depends on the approved specification and application conditions.
Where is Transformer Spade Terminals, Transformer Spade Connectors commonly used?
Typical applications include power distribution, grounding and cable termination. Confirm load, environment, mating parts and applicable standards before selection.
Which materials are available for Transformer Spade Terminals, Transformer Spade Connectors?
Specify conductive brass, copper, bronze or aluminium. State the exact grade because similar commercial alloys can differ in composition and performance.
Which sizes can be supplied for Transformer Spade Terminals, Transformer Spade Connectors?
Standard and custom sizes can be reviewed from conductor range, stud or thread size, contact area and mounting dimensions. Nominal size alone may not define compatibility.
What dimensions are required to order Transformer Spade Terminals, Transformer Spade Connectors?
Provide conductor range, stud or thread size, contact area and mounting dimensions, with units, tolerances and drawing revision.
Can Transformer Spade Terminals, Transformer Spade Connectors be made to a custom drawing?
Yes. Custom geometry, threads, tolerances and features can be assessed from a dimensioned drawing or approved sample.
Which thread standards are available for Transformer Spade Terminals, Transformer Spade Connectors?
Relevant Metric, BSP, BSPT, NPT, NPTF, PG, BA or BSW threads may be considered. Specify form, size, pitch, class and engagement length.
Which finishes are offered for Transformer Spade Terminals, Transformer Spade Connectors?
Options may include natural, tin-plated or nickel-plated. Specify coating type, thickness, appearance and corrosion or conductivity needs.
What tolerances can be maintained on Transformer Spade Terminals, Transformer Spade Connectors?
Tolerance depends on material, size, geometry and process. Mark critical dimensions and fits clearly on the drawing.
How should Transformer Spade Terminals, Transformer Spade Connectors be installed?
Check mating dimensions, orientation, sealing or retention method and specified tightening torque before use.
How is Transformer Spade Terminals, Transformer Spade Connectors inspected?
Inspection can cover material identity, critical dimensions, threads, finish and drawing-specific functional checks.
Which quality documents are available for Transformer Spade Terminals, Transformer Spade Connectors?
Material certificates, dimensional reports and coating or test records can be agreed at quotation stage.
Are samples available for Transformer Spade Terminals, Transformer Spade Connectors?
Prototype or pre-production samples can be reviewed for new custom parts, subject to tooling and material requirements.
What are the MOQ and lead time for Transformer Spade Terminals, Transformer Spade Connectors?
Minimum quantity and lead time vary with material, size, tooling, finish, inspection and order volume.
What is needed for a Transformer Spade Terminals, Transformer Spade Connectors quotation?
Provide the drawing or specification, material, dimensions, tolerances, finish, quantity, inspection, packing and destination.