CZ 121 Brass Turned Parts and Machined Components
Brass Parts India offers cz 121 brass turned parts and machined components for drawing-based industrial manufacture and supply from Jamnagar, India. The range serves electrical OEMs, EPC contractors, power utilities and distributors sourcing precision bushings, connector pins, threaded inserts, spacers and custom fittings. Specify CZ121Pb3 / CuZn39Pb3 family, the applicable raw-material standard, finished dimensions, quantity and inspection requirements for an engineering review and quotation.
Price: US$ 13.90/kg
Request an order-specific quotation confirming the weight basis, tooling, finishing, delivery and applicable charges.
Product overview
CZ121 free-cutting brass for drawing-based manufacture
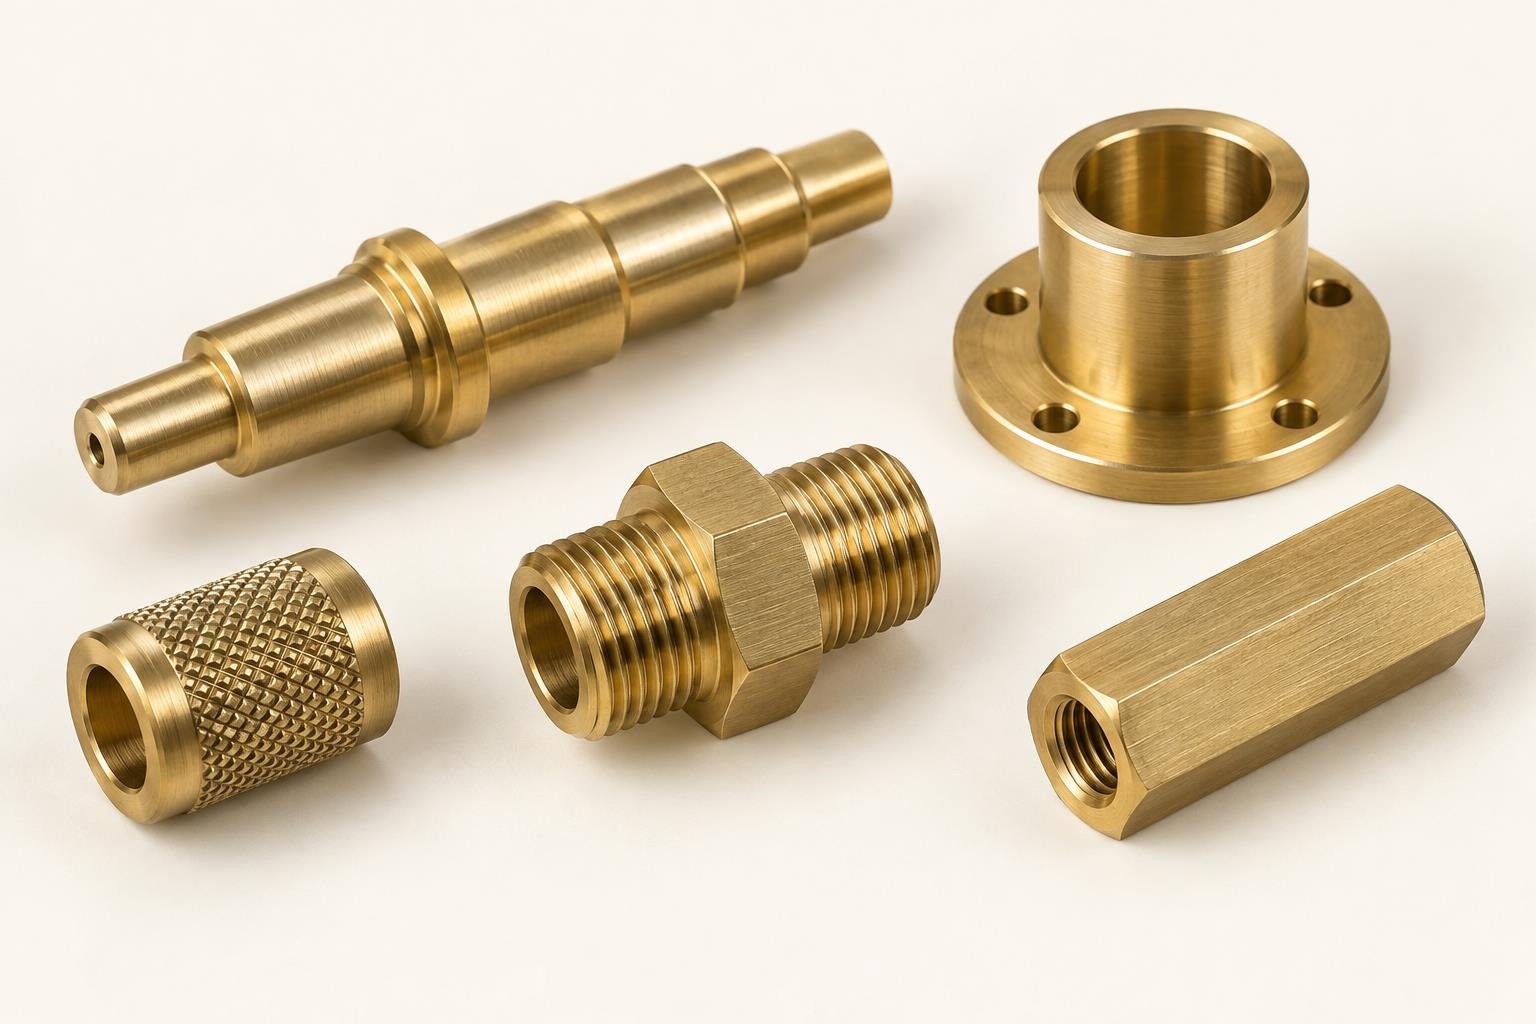
CZ121 brass turned parts are components produced from free-machining copper-zinc-lead alloy to a controlled engineering drawing. The commercial designation is widely used on British legacy drawings for bushes, inserts, spacers, threaded connectors and small precision fasteners. For a new order, the drawing should identify the complete material specification, lead variant and supply condition. Brass Parts India accepts enquiries for custom machined components where dimensional fit, thread engagement, surface condition and repeatability matter more than the appearance of the unfinished bar.
Legacy CZ121 drawings and modern material selection
A drawing marked only CZ121 may omit information needed for present-day material purchasing. CZ121Pb3 is commonly cross-referenced with CW614N and CuZn39Pb3, while CZ121Pb4 belongs to a different lead-content family. The original British product standard and drawing revision should therefore be reviewed before placing an order. A proposed replacement needs acceptance against composition, temper, mechanical properties and product form. Changing the alloy on a purchase order without updating the drawing creates avoidable ambiguity for incoming inspection and future repeat batches.
Turned bushes, sleeves and precision shoulders
Cylindrical CZ121 parts can combine an outside diameter, concentric bore, shoulder, recess and flange in one component. These features locate mating parts, maintain separation or provide a replaceable guiding surface when the assembly design permits. Functional datums should connect the features that actually control fit. A bore tolerance alone does not define alignment to an outside seat. Drawings should also specify edge breaks, bore finish, allowable tool witness marks and the dimensions that must be checked after any plating operation.
Knurled inserts and threaded machined components
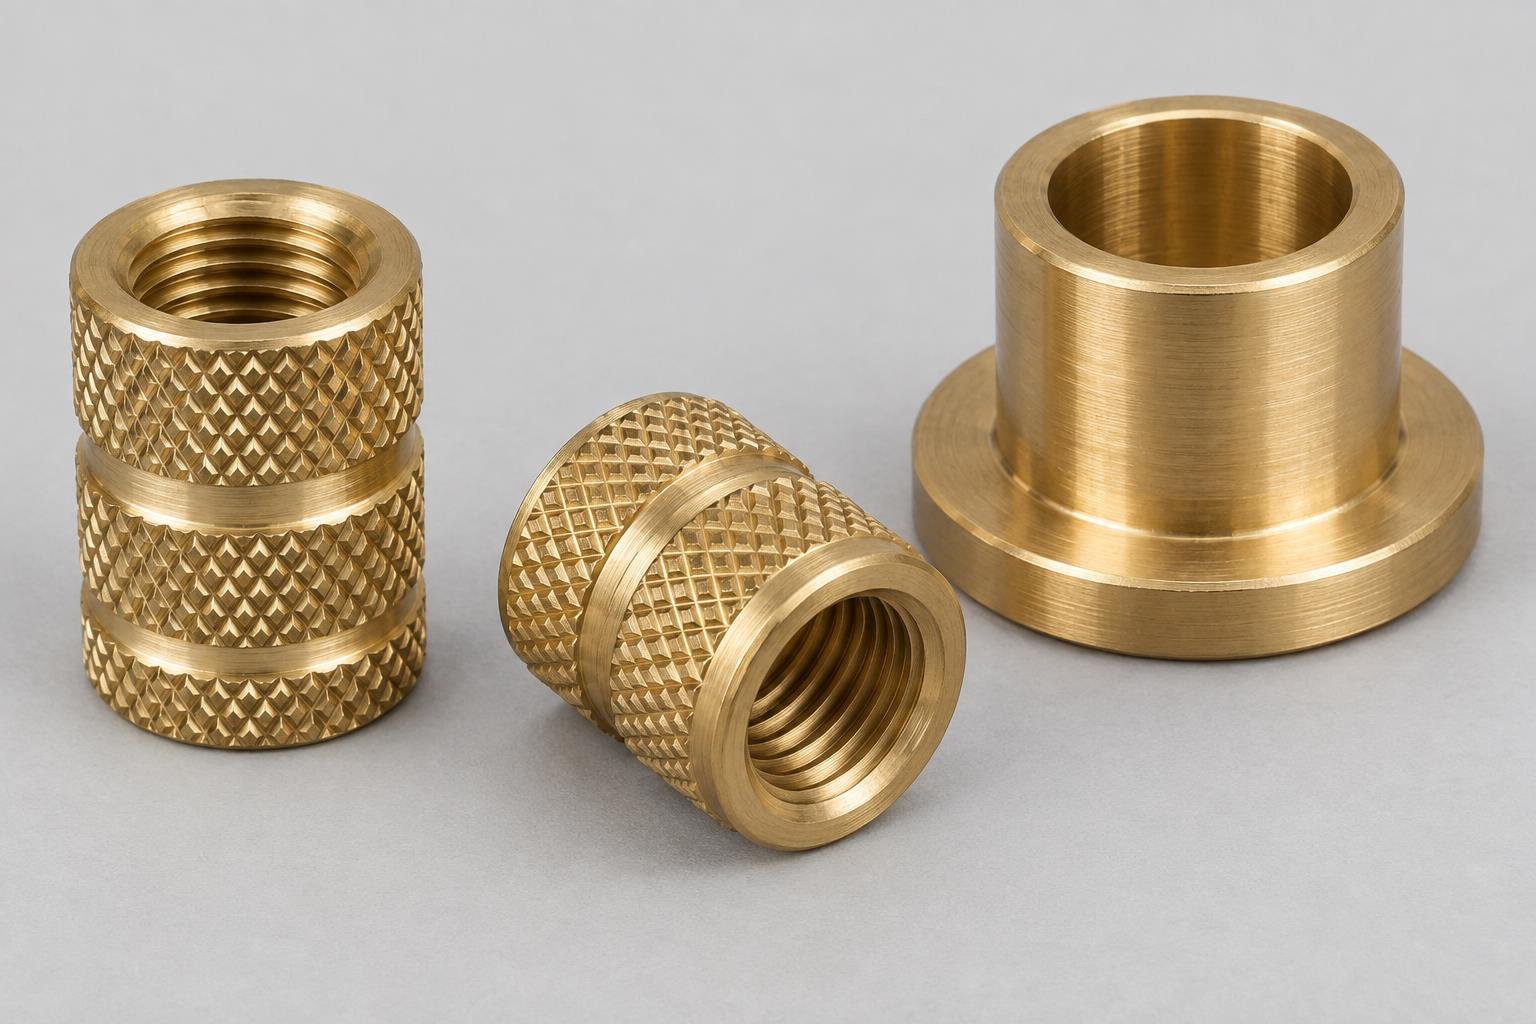
CZ121 is frequently considered for machined inserts because free-cutting behaviour supports the production of small threads and detailed exterior profiles. Straight knurls, diamond knurls, undercuts and flange geometries provide different retention mechanisms in the surrounding material. The correct pattern depends on whether the insert is moulded in, pressed in or installed by another method. Pull-out and torque resistance belong to the complete insert-and-host-material system. They must be qualified using the actual resin, wall thickness, installation process and operating temperature.
Electrical OEM components and contact interfaces
Machined brass pins, terminal bodies, contact screws and connector sleeves can bring several assembly features into a single compact part. For electrical use, the buyer should specify conductor size, clamping method, interface pressure and any permitted temperature rise. Brass has lower electrical conductivity than high-conductivity copper, so section size and contact geometry require engineering review. Nickel or tin finishes may be requested where compatible with the connection. Neither the alloy name nor a bright plated appearance establishes a current rating for the finished assembly.
Batch supply for maintenance and distribution
Distributors and maintenance buyers often need CZ121 parts that match an installed assembly and an older part number. A sample can help identify visible geometry, but it cannot reliably establish material chemistry or original tolerances. The enquiry should include a drawing, required batch quantity and any accepted substitute grades. Identify which features are functionally critical and which are cosmetic. Keeping an approved sample, drawing revision and inspection requirements together helps purchasing teams reorder the same component without relying on informal descriptions or visual similarity.
Key features
- Custom component geometry based on controlled drawings and specifications.
- Material selection identified by grade, product standard and required condition.
- Turning, drilling, threading and secondary features reviewed for the part.
- Natural brass, electro-tinned or nickel finish options by agreement.
- Metric and imperial thread requirements supported by complete callouts.
- Inspection scope and repeat-order identification agreed before manufacture.
Drawing-controlled dimensions
Turned diameters, bores, shoulders and seating faces can be specified around the functional requirements of the assembly. Identify the datum from which each critical feature is measured, then define the fit or geometric control needed at the mating interface. Tolerances should be realistic for the part length, wall thickness and finishing route. Agree which dimensions are checked on every batch and which require additional sampling. This creates an inspection plan that supports assembly performance without treating every decorative or clearance surface as equally critical.
Internal and external thread options
Threaded brass components can be specified with metric or imperial threads to suit existing equipment. The parent product range lists ISO metric, BSW, BA, BSF, UNC, UNF and UNEF options. Each order should name the thread standard, pitch, tolerance class, engagement and any required relief. For plated parts, state whether gauging applies after coating. Blind holes also need a usable thread depth and drill-depth limit. A complete thread callout prevents confusion between nominal thread length and the portion that can carry the mating fastener.
Machined surface finish and edge control
Surface roughness should be stated where it affects sealing, sliding, contact or appearance. A smooth-looking surface is not a measurement, and a general finish note may not identify the critical location. Chamfers and radii help assembly but must not remove necessary thread engagement or sealing area. Cross holes, slots and internal intersections deserve specific burr checks. Define acceptable edge treatment on the drawing so that deburring removes loose material while preserving the designed geometry, especially around small contact pins and thin machined sleeves.
Natural brass, tin and nickel finishes
The finish families on the parent range include natural brass, electro-tinned and nickel surfaces. Select a coating for its intended function and compatibility with the mating material. Specify coating thickness, areas to be masked, appearance criteria and any adhesion or corrosion test required by the equipment specification. Coatings alter dimensions and may affect thread fit, solderability or electrical contact behaviour. Approve the finished condition using representative samples, rather than assuming that an uncoated dimensional report proves conformity of the plated production part.
Part identification and repeat-order control
Stable repeat supply starts with a consistent part number and drawing revision. Include the ordered material, approved finish, batch quantity and packaging requirements on the purchase order. If marking the component is impractical, agree an appropriate label and batch identification method. Keep similar variants separated, particularly when they differ only in bore size, thread pitch or plating. For distributors, a clear stock description should distinguish the alloy from the component type. This reduces the chance that visually similar hardware is issued against the wrong customer specification.
Technical specifications
| Parameter | Specification / ordering requirement |
|---|---|
| Product material | CZ121Pb3 / CuZn39Pb3 family |
| Raw-material specification | Legacy BS grade; confirm Pb3 or Pb4 variant |
| Manufacturing route | Bar turning with drilling, boring, threading and secondary machining as required |
| Size envelope | Parent range lists 1 mm to 200 mm; feasibility for this grade and geometry is confirmed at quotation |
| Tolerance and roughness | Drawing-specific; identify final dimensions after plating |
| Threads | ISO metric, BSW, BA, BSF, UNC, UNF, UNEF; standard and class as ordered |
| Finish | Natural brass, electro-tinned or nickel; thickness and acceptance by agreement |
| Mechanical properties | Dependent on stock size, temper and specification; confirm with material documentation |
| Quantity and lead time | Confirmed for the drawing, stock availability and batch size |
| Listed rate | US$ 13.90/kg |
Raw-material grade selection
The following families cover common machining and forging enquiries. They are selection references, not a claim that one alloy can replace another. Nominal chemical symbols describe alloy families; the ordered standard and material certificate establish the accepted composition limits. Restricted supplier compositions and older standard editions may use different limits. Do not infer a batch analysis from the nominal symbol.
| Grade family | Nominal / commercial reference | Primary selection consideration |
|---|---|---|
| CZ121Pb3 / CW614N | CuZn39Pb3 | Free machining of turned components; distinguish any Pb4 requirement |
| C36000 / CW603N | CuZn36Pb3 comparison family | Machined pins, sleeves and screw-machine components; compare standard limits |
| C37700 / CW612N | CuZn39Pb2 comparison family | Hot-formed blanks requiring subsequent machining |
| CW617N | CuZn40Pb2 | Related forging-brass option requiring design and specification approval |
| Lead-free or DZR brass | Specific grade must be separately nominated | Alternative selection where lead limits or dezincification resistance control the application |
International equivalents and comparison terms
| European reference | Legacy British reference | Common UNS comparison | Acceptance note |
|---|---|---|---|
| CW614N / CuZn39Pb3 | CZ121Pb3 | C38500 | Compare chemistry, temper and product form |
| CW603N / CuZn36Pb3 | CZ124 | C36000 | Related machining family; not automatic dual certification |
| CW612N / CuZn39Pb2 | CZ128 | C37700 | Related forging family; verify the ordered standard |
| CW617N / CuZn40Pb2 | CZ122 | No direct substitute asserted here | Different forging alloy; requires approval |
Product types and variants
| Component type | Typical design features | Define on the drawing |
|---|---|---|
| Bushings and sleeves | Plain bore, shoulder, flange or recess | Fit, bore alignment, wall thickness and edge breaks |
| Pins and terminals | Stepped diameters, contact faces or cross holes | Mating geometry, conductor interface and final finish |
| Inserts and standoffs | Internal thread, knurl, groove or external thread | Host material, installation route and retention requirement |
| Adapters and connectors | Wrench flats, bore, thread or sealing face | Thread standard, engagement and sealing method |
| Custom bodies | Offset holes, bosses, slots or mounting surfaces | Datum scheme, machining allowance and inspection plan |
Applications in industry
| Customer / sector | Typical component enquiries | Engineering requirement |
|---|---|---|
| Electrical OEMs | Pins, terminal screws, sleeves and connector bodies | Contact geometry, temperature rise and assembly validation |
| EPC contractors | Panel spacers, fastening details and specified connection parts | Approved project drawing and destination requirements |
| Power utilities | Equipment repair parts, terminals and mounting components | Approved material and equipment-level qualification |
| Industrial distributors | Repeat turned parts, inserts, adapters and custom hardware | Part identification, packaging and controlled substitutions |
| Instrumentation and machinery | Bushings, collars, precision spacers and threaded interfaces | Fit, alignment, service environment and wear assessment |
Application names indicate where enquiries arise; they do not establish a rating for every part in the range. Define installation loads, operating temperature, corrosion exposure and maintenance needs. Where a component enters regulated equipment, specify the relevant approval and testing requirements before design release. For replacement supply, verify the original drawing and equipment requirements rather than selecting solely by the appearance of a sample.
Manufacturing process
1. Drawing review and stock selection
Manufacture begins by reviewing the drawing revision, material standard, dimensions, finish and order quantity. The review identifies critical datums, thread requirements and inspection records. Stock form and condition are selected for the approved production route. For a forged component, the blank design additionally needs draft, radii, parting-line placement and machining allowance. Any material substitution should be resolved before stock is released to production.
2. Forming and precision machining
Turning produces the principal diameters, shoulders and faces from suitable stock. Drilling, boring and threading create internal features, and secondary operations add flats, cross holes or slots. The sequence is chosen to maintain the relationship between functional surfaces. Slender sections, deep holes and interrupted cuts need appropriate support and tooling. Process settings are established for the actual part rather than copied from a generic alloy description.
3. Finishing, inspection and packing
Deburring and cleaning remove loose edges and machining residue before final inspection or the agreed surface treatment. When plating is required, final dimensions and thread fit should be verified in the finished condition. The inspection scope follows the order requirements. Packaging then protects surfaces and maintains part identification through dispatch, receiving inspection and storage. Special cleanliness or individually separated packing should be stated at enquiry stage.
Quality standards and certifications
Brass Parts India describes material inspection, manufacturing checks, testing and final inspection in its quality policy. For this product, acceptance should be based on the ordered raw-material standard, approved drawing and agreed inspection plan. References to ASTM, EN or legacy BS specifications describe requirements to be specified; they are not claims of third-party product certification.
| Document / check | What to request |
|---|---|
| Material certificate | Grade, material standard, batch identity and relevant test results |
| Dimensional report | Critical drawing features and measurement results |
| Thread inspection | Applicable standard, tolerance class and agreed gauges |
| Finish evidence | Coating specification and agreed checks, where ordered |
| Management or product certification | Request the current certificate and confirm its scope when your supplier approval requires it |
Do not infer ISO 9001, UL, CE, drinking-water approval or a universal compliance status from this page. Certification and regulatory requirements are application-specific and should be confirmed with current documentation for the order. These leaded grades are not lead-free alloys. If restrictions apply to the destination or finished equipment, include them in the enquiry so material selection and compliance evidence can be reviewed.
Why choose Brass Parts India
Brass Parts India provides a focused source for custom brass and copper component enquiries from Jamnagar, India. Its turned-parts range includes drawing-based manufacture, multiple thread families and natural or plated finishes. Buyers can discuss the required component geometry together with related turned and pressed parts in the same product category. This is useful when one assembly contains several small components with different manufacturing routes.
The practical basis for supplier selection is a clear quotation, an agreed drawing and appropriate evidence of conformity. Send the functional requirements early so material, finish and inspection can be coordinated. For an OEM programme, identify expected repeat quantities and approval samples. For project procurement, include destination and delivery milestones. For distribution, specify stock labels and packaging. The quotation should state the confirmed supply scope and any unresolved technical points before the order is placed.
Frequently Asked Questions – CZ 121 Brass Turned Parts and Machined Components
What is CZ 121 Brass Turned Parts and Machined Components?
CZ 121 Brass Turned Parts and Machined Components is a precision engineered component used in industrial machinery, electrical equipment and OEM assemblies. Final suitability depends on the approved specification and application conditions.
Where is CZ 121 Brass Turned Parts and Machined Components commonly used?
Typical applications include industrial machinery, electrical equipment and OEM assemblies. Confirm load, environment, mating parts and applicable standards before selection.
Which materials are available for CZ 121 Brass Turned Parts and Machined Components?
Specify the drawing-specified brass, copper, aluminium or stainless steel grade. State the exact grade because similar commercial alloys can differ in composition and performance.
Which sizes can be supplied for CZ 121 Brass Turned Parts and Machined Components?
Standard and custom sizes can be reviewed from drawing dimensions, datums, threads, tolerances and surface finish. Nominal size alone may not define compatibility.
What dimensions are required to order CZ 121 Brass Turned Parts and Machined Components?
Provide drawing dimensions, datums, threads, tolerances and surface finish, with units, tolerances and drawing revision.
Can CZ 121 Brass Turned Parts and Machined Components be made to a custom drawing?
Yes. Custom geometry, threads, tolerances and features can be assessed from a dimensioned drawing or approved sample.
Which thread standards are available for CZ 121 Brass Turned Parts and Machined Components?
Relevant Metric, BSP, BSPT, NPT, NPTF, PG, BA or BSW threads may be considered. Specify form, size, pitch, class and engagement length.
Which finishes are offered for CZ 121 Brass Turned Parts and Machined Components?
Options may include machined, polished, plated, passivated or anodised. Specify coating type, thickness, appearance and corrosion or conductivity needs.
What tolerances can be maintained on CZ 121 Brass Turned Parts and Machined Components?
Tolerance depends on material, size, geometry and process. Mark critical dimensions and fits clearly on the drawing.
How should CZ 121 Brass Turned Parts and Machined Components be installed?
Check mating dimensions, orientation, sealing or retention method and specified tightening torque before use.
How is CZ 121 Brass Turned Parts and Machined Components inspected?
Inspection can cover material identity, critical dimensions, threads, finish and drawing-specific functional checks.
Which quality documents are available for CZ 121 Brass Turned Parts and Machined Components?
Material certificates, dimensional reports and coating or test records can be agreed at quotation stage.
Are samples available for CZ 121 Brass Turned Parts and Machined Components?
Prototype or pre-production samples can be reviewed for new custom parts, subject to tooling and material requirements.
What are the MOQ and lead time for CZ 121 Brass Turned Parts and Machined Components?
Minimum quantity and lead time vary with material, size, tooling, finish, inspection and order volume.
What is needed for a CZ 121 Brass Turned Parts and Machined Components quotation?
Provide the drawing or specification, material, dimensions, tolerances, finish, quantity, inspection, packing and destination.