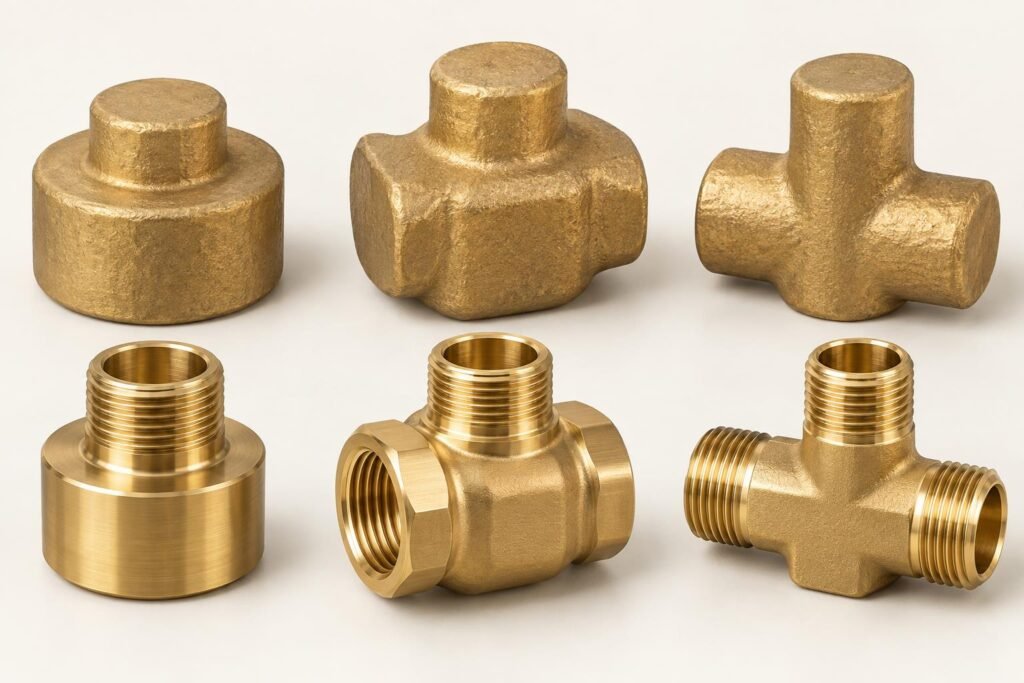
CW614N (CuZn39Pb3) Brass Turned Parts
Brass Parts India offers cw614n (cuzn39pb3) brass turned parts for drawing-based industrial manufacture and supply from Jamnagar, India. The range serves electrical OEMs, EPC contractors, power utilities and distributors sourcing precision bushings, connector pins, threaded inserts, spacers and custom fittings. Specify CW614N / CuZn39Pb3, the applicable raw-material standard, finished dimensions, quantity and inspection requirements for an engineering review and quotation.
Price: US$ 13.90/kg
Request an order-specific quotation confirming the weight basis, tooling, finishing, delivery and applicable charges.
Product overview
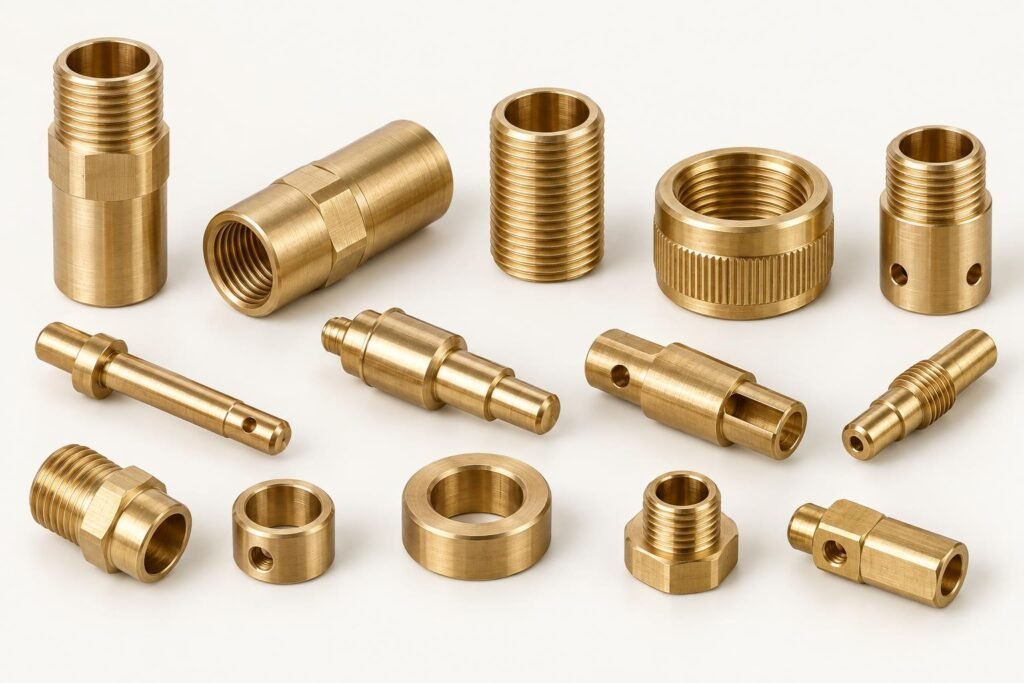
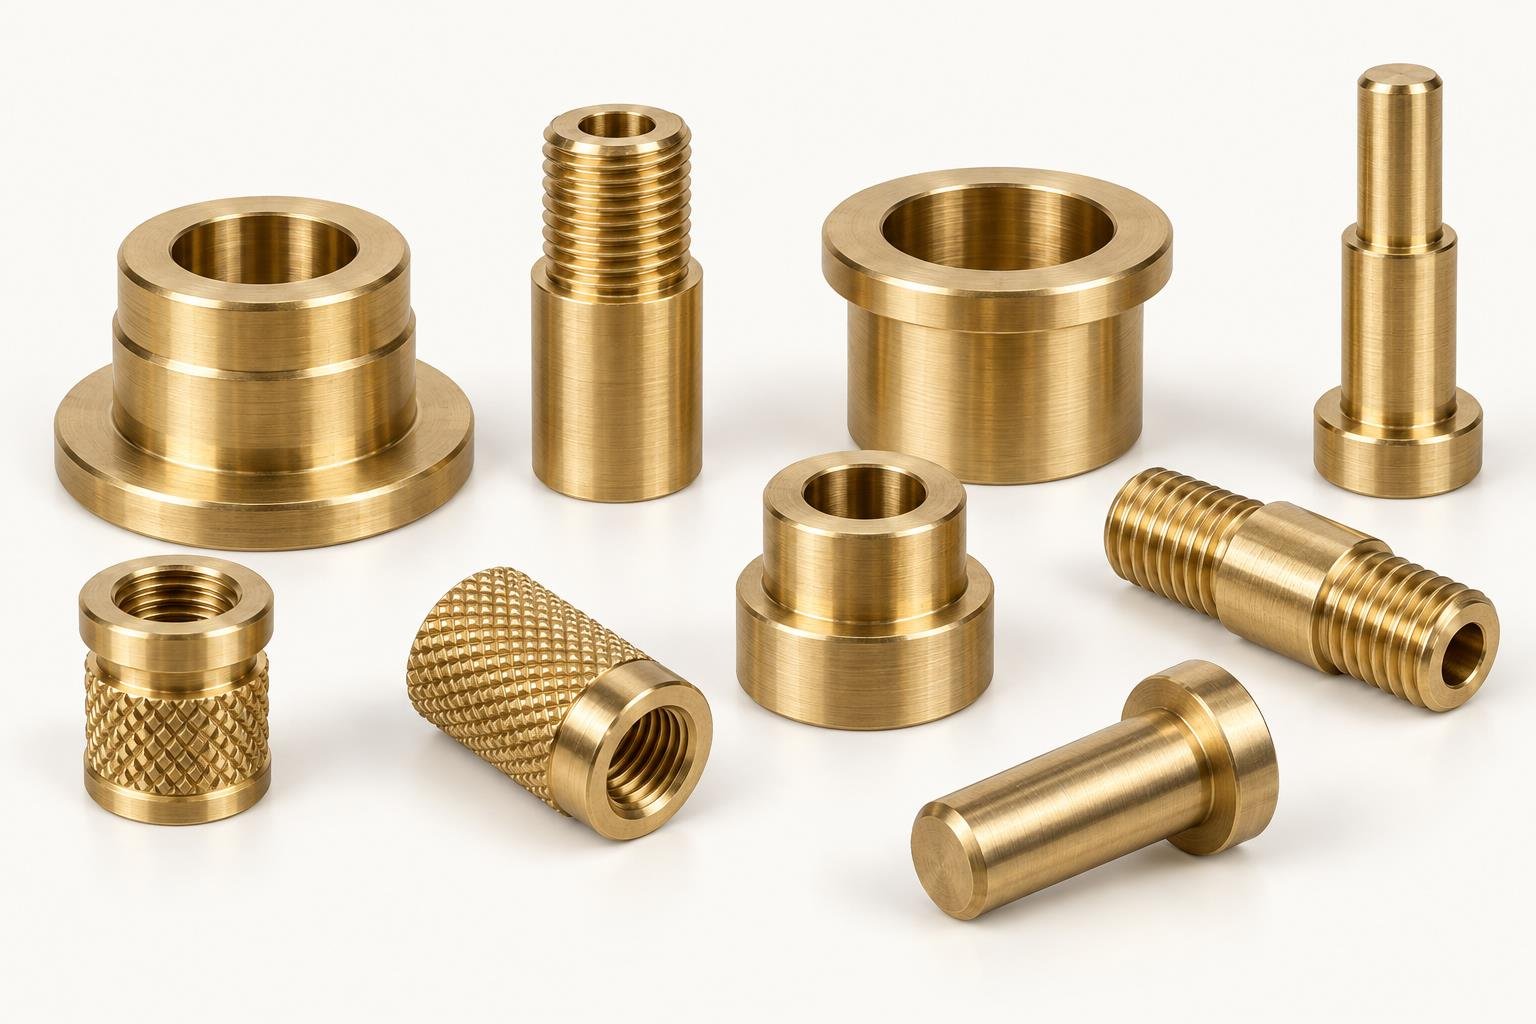
CW614N precision turned components
CW614N is the European material number for CuZn39Pb3, a leaded brass used extensively for free-machining applications. Turned components include bushings, threaded inserts, spacers, adapters, collars and small fasteners made to an engineering drawing. Brass Parts India accepts custom-part enquiries from electrical OEMs, EPC contractors, utilities and distributors. A usable specification combines the material number with a product standard, supply condition and dimensional requirements. The component drawing then controls the geometry and functional interfaces of the delivered part.
CuZn39Pb3 chemistry and purchasing identity
The chemical symbol CuZn39Pb3 describes the nominal alloy family rather than an exact batch analysis. Zinc is the balance after copper, lead and permitted minor elements are accounted for. EN 12164 is a relevant specification for free-machining rod, while other product forms use their applicable standards. A mill certificate should be checked against the ordered grade and edition. Chemical conformity alone does not establish the temper, tensile properties or dimensional tolerances needed for a specific stock size and finished component.
Precision shoulders and concentric turned surfaces
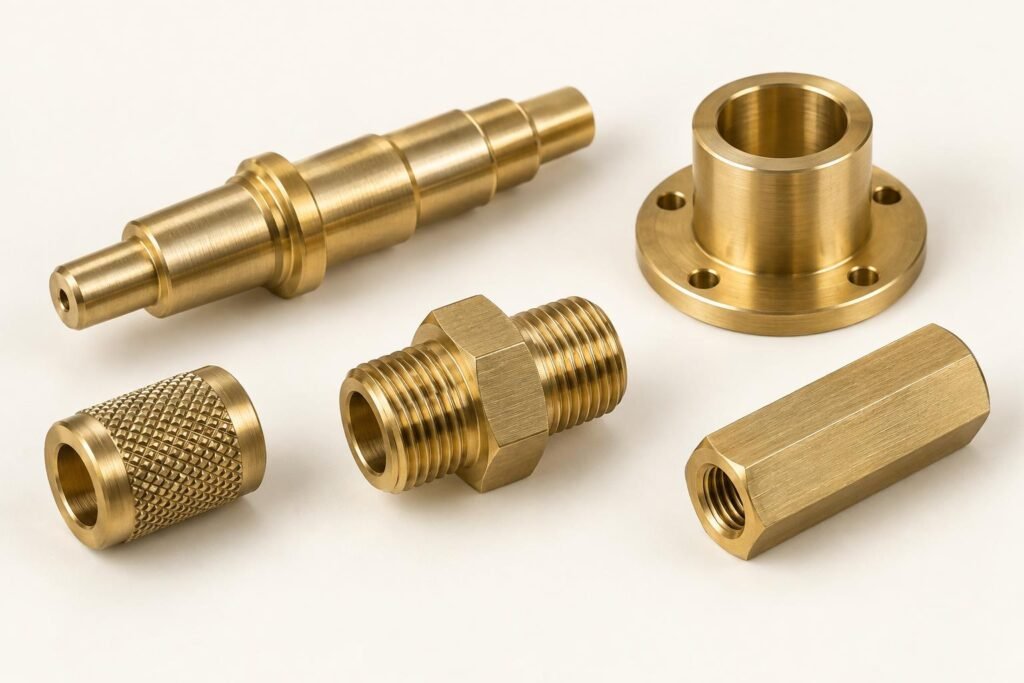
CW614N is useful for parts in which a bore, outside seat and shoulder must work together. The drawing should state the datum scheme and any runout, perpendicularity or positional requirement that controls assembly function. Excessively tight tolerances on nonfunctional surfaces can increase manufacturing effort without improving the product. A review should concentrate control on mating features, sealing interfaces and areas that determine alignment. Distinguishing these requirements helps both the producer and receiving inspector use the same practical definition of an acceptable component.
Insert geometry and repeat assembly
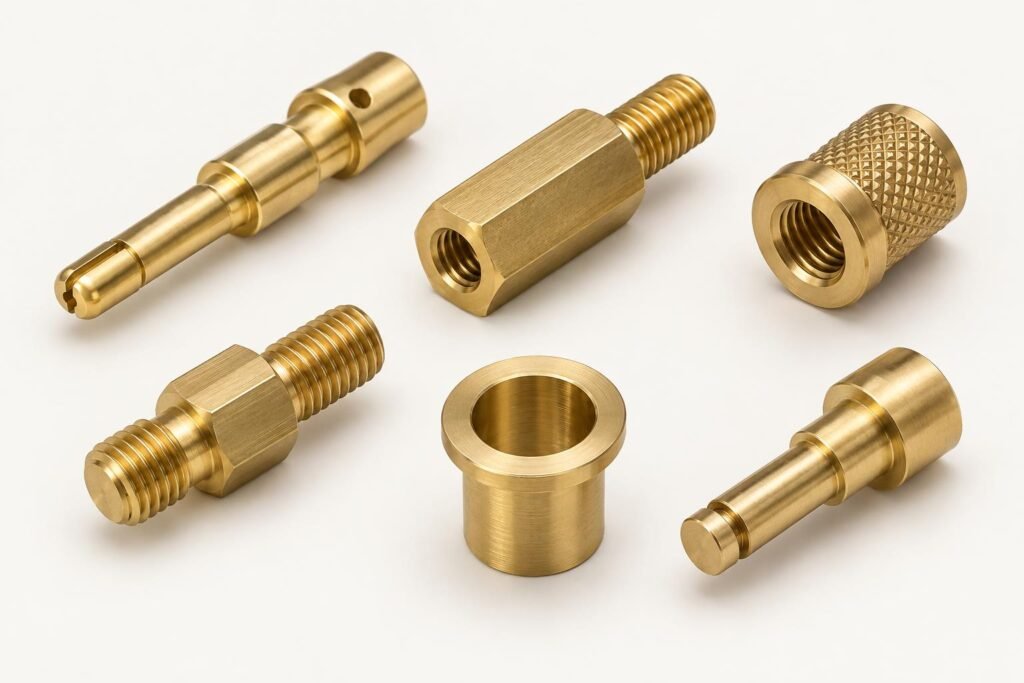
Threaded inserts and standoffs made from CW614N may incorporate external knurls, grooves or shoulders for retention. The correct configuration depends on the host material, installation method and available wall thickness. A larger knurl does not necessarily improve retention if it damages the surrounding material or reduces the insert wall. Thread quality, burr control and lead-in geometry influence assembly consistency. Qualification of torque-out, pull-out and repeated tightening should use production-representative parts in the actual mating material and installation process.
European drawings and legacy CZ121 references
CW614N is commonly cross-referenced to CZ121Pb3 and the older CuZn39Pb3 material naming system. This relationship helps interpret legacy drawings, but the original specification still matters. Some drawings state CZ121 without a lead variant, and that omission should be resolved before purchasing material. C38500 also appears in commercial comparison tables for this family, whereas C36000 belongs to a different comparison group. A material change should be documented and accepted, especially where an OEM maintains an approved material list.
Industrial supply and finish coordination
CW614N parts can be requested with natural brass surfaces or suitable plated finishes for the intended equipment. Surface preparation, coating thickness and coverage must be coordinated with thread and bore tolerances. A plated sleeve may fit differently from an uncoated approval sample even when both were machined to the same dimensions. State final dimensions after finishing and identify surfaces that need masking. Packing should protect small machined edges and keep distinct part numbers separated so that correct parts remain identifiable during incoming inspection and assembly.
Key features
- Custom component geometry based on controlled drawings and specifications.
- Material selection identified by grade, product standard and required condition.
- Turning, drilling, threading and secondary features reviewed for the part.
- Natural brass, electro-tinned or nickel finish options by agreement.
- Metric and imperial thread requirements supported by complete callouts.
- Inspection scope and repeat-order identification agreed before manufacture.
Drawing-controlled dimensions
Turned diameters, bores, shoulders and seating faces can be specified around the functional requirements of the assembly. Identify the datum from which each critical feature is measured, then define the fit or geometric control needed at the mating interface. Tolerances should be realistic for the part length, wall thickness and finishing route. Agree which dimensions are checked on every batch and which require additional sampling. This creates an inspection plan that supports assembly performance without treating every decorative or clearance surface as equally critical.
Internal and external thread options
Threaded brass components can be specified with metric or imperial threads to suit existing equipment. The parent product range lists ISO metric, BSW, BA, BSF, UNC, UNF and UNEF options. Each order should name the thread standard, pitch, tolerance class, engagement and any required relief. For plated parts, state whether gauging applies after coating. Blind holes also need a usable thread depth and drill-depth limit. A complete thread callout prevents confusion between nominal thread length and the portion that can carry the mating fastener.
Machined surface finish and edge control
Surface roughness should be stated where it affects sealing, sliding, contact or appearance. A smooth-looking surface is not a measurement, and a general finish note may not identify the critical location. Chamfers and radii help assembly but must not remove necessary thread engagement or sealing area. Cross holes, slots and internal intersections deserve specific burr checks. Define acceptable edge treatment on the drawing so that deburring removes loose material while preserving the designed geometry, especially around small contact pins and thin machined sleeves.
Natural brass, tin and nickel finishes
The finish families on the parent range include natural brass, electro-tinned and nickel surfaces. Select a coating for its intended function and compatibility with the mating material. Specify coating thickness, areas to be masked, appearance criteria and any adhesion or corrosion test required by the equipment specification. Coatings alter dimensions and may affect thread fit, solderability or electrical contact behaviour. Approve the finished condition using representative samples, rather than assuming that an uncoated dimensional report proves conformity of the plated production part.
Part identification and repeat-order control
Stable repeat supply starts with a consistent part number and drawing revision. Include the ordered material, approved finish, batch quantity and packaging requirements on the purchase order. If marking the component is impractical, agree an appropriate label and batch identification method. Keep similar variants separated, particularly when they differ only in bore size, thread pitch or plating. For distributors, a clear stock description should distinguish the alloy from the component type. This reduces the chance that visually similar hardware is issued against the wrong customer specification.
Technical specifications
| Parameter | Specification / ordering requirement |
|---|---|
| Product material | CW614N / CuZn39Pb3 |
| Raw-material specification | EN 12164 free-machining rod, as ordered |
| Manufacturing route | Bar turning with drilling, boring, threading and secondary machining as required |
| Size envelope | Parent range lists 1 mm to 200 mm; feasibility for this grade and geometry is confirmed at quotation |
| Tolerance and roughness | Drawing-specific; identify final dimensions after plating |
| Threads | ISO metric, BSW, BA, BSF, UNC, UNF, UNEF; standard and class as ordered |
| Finish | Natural brass, electro-tinned or nickel; thickness and acceptance by agreement |
| Mechanical properties | Dependent on stock size, temper and specification; confirm with material documentation |
| Quantity and lead time | Confirmed for the drawing, stock availability and batch size |
| Listed rate | US$ 13.90/kg |
Raw-material grade selection
The following families cover common machining and forging enquiries. They are selection references, not a claim that one alloy can replace another. Nominal chemical symbols describe alloy families; the ordered standard and material certificate establish the accepted composition limits. Restricted supplier compositions and older standard editions may use different limits. Do not infer a batch analysis from the nominal symbol.
| Grade family | Nominal / commercial reference | Primary selection consideration |
|---|---|---|
| CZ121Pb3 / CW614N | CuZn39Pb3 | Free machining of turned components; distinguish any Pb4 requirement |
| C36000 / CW603N | CuZn36Pb3 comparison family | Machined pins, sleeves and screw-machine components; compare standard limits |
| C37700 / CW612N | CuZn39Pb2 comparison family | Hot-formed blanks requiring subsequent machining |
| CW617N | CuZn40Pb2 | Related forging-brass option requiring design and specification approval |
| Lead-free or DZR brass | Specific grade must be separately nominated | Alternative selection where lead limits or dezincification resistance control the application |
International equivalents and comparison terms
| European reference | Legacy British reference | Common UNS comparison | Acceptance note |
|---|---|---|---|
| CW614N / CuZn39Pb3 | CZ121Pb3 | C38500 | Compare chemistry, temper and product form |
| CW603N / CuZn36Pb3 | CZ124 | C36000 | Related machining family; not automatic dual certification |
| CW612N / CuZn39Pb2 | CZ128 | C37700 | Related forging family; verify the ordered standard |
| CW617N / CuZn40Pb2 | CZ122 | No direct substitute asserted here | Different forging alloy; requires approval |
Product types and variants
| Component type | Typical design features | Define on the drawing |
|---|---|---|
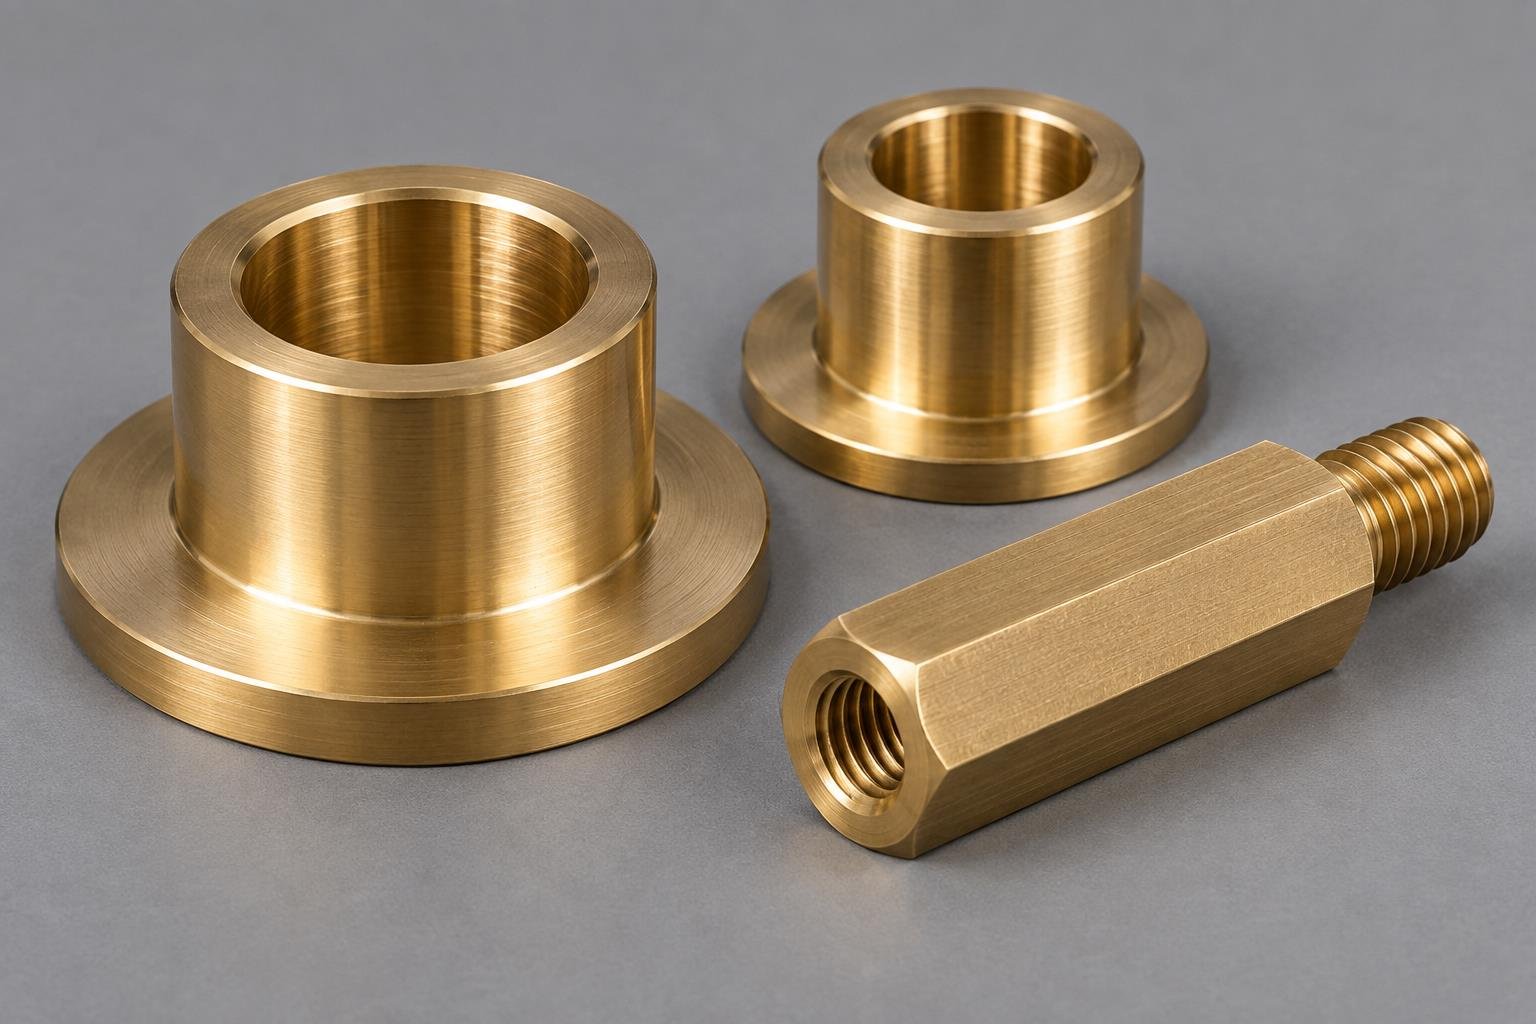
| Bushings and sleeves | Plain bore, shoulder, flange or recess | Fit, bore alignment, wall thickness and edge breaks |
| Pins and terminals | Stepped diameters, contact faces or cross holes | Mating geometry, conductor interface and final finish |
| Inserts and standoffs | Internal thread, knurl, groove or external thread | Host material, installation route and retention requirement |
| Adapters and connectors | Wrench flats, bore, thread or sealing face | Thread standard, engagement and sealing method |
| Custom bodies | Offset holes, bosses, slots or mounting surfaces | Datum scheme, machining allowance and inspection plan |
Applications in industry
| Customer / sector | Typical component enquiries | Engineering requirement |
|---|---|---|
| Electrical OEMs | Pins, terminal screws, sleeves and connector bodies | Contact geometry, temperature rise and assembly validation |
| EPC contractors | Panel spacers, fastening details and specified connection parts | Approved project drawing and destination requirements |
| Power utilities | Equipment repair parts, terminals and mounting components | Approved material and equipment-level qualification |
| Industrial distributors | Repeat turned parts, inserts, adapters and custom hardware | Part identification, packaging and controlled substitutions |
| Instrumentation and machinery | Bushings, collars, precision spacers and threaded interfaces | Fit, alignment, service environment and wear assessment |
Application names indicate where enquiries arise; they do not establish a rating for every part in the range. Define installation loads, operating temperature, corrosion exposure and maintenance needs. Where a component enters regulated equipment, specify the relevant approval and testing requirements before design release. For replacement supply, verify the original drawing and equipment requirements rather than selecting solely by the appearance of a sample.
Manufacturing process
1. Drawing review and stock selection
Manufacture begins by reviewing the drawing revision, material standard, dimensions, finish and order quantity. The review identifies critical datums, thread requirements and inspection records. Stock form and condition are selected for the approved production route. For a forged component, the blank design additionally needs draft, radii, parting-line placement and machining allowance. Any material substitution should be resolved before stock is released to production.
2. Forming and precision machining
Turning produces the principal diameters, shoulders and faces from suitable stock. Drilling, boring and threading create internal features, and secondary operations add flats, cross holes or slots. The sequence is chosen to maintain the relationship between functional surfaces. Slender sections, deep holes and interrupted cuts need appropriate support and tooling. Process settings are established for the actual part rather than copied from a generic alloy description.
3. Finishing, inspection and packing
Deburring and cleaning remove loose edges and machining residue before final inspection or the agreed surface treatment. When plating is required, final dimensions and thread fit should be verified in the finished condition. The inspection scope follows the order requirements. Packaging then protects surfaces and maintains part identification through dispatch, receiving inspection and storage. Special cleanliness or individually separated packing should be stated at enquiry stage.
Quality standards and certifications
Brass Parts India describes material inspection, manufacturing checks, testing and final inspection in its quality policy. For this product, acceptance should be based on the ordered raw-material standard, approved drawing and agreed inspection plan. References to ASTM, EN or legacy BS specifications describe requirements to be specified; they are not claims of third-party product certification.
| Document / check | What to request |
|---|---|
| Material certificate | Grade, material standard, batch identity and relevant test results |
| Dimensional report | Critical drawing features and measurement results |
| Thread inspection | Applicable standard, tolerance class and agreed gauges |
| Finish evidence | Coating specification and agreed checks, where ordered |
| Management or product certification | Request the current certificate and confirm its scope when your supplier approval requires it |
Do not infer ISO 9001, UL, CE, drinking-water approval or a universal compliance status from this page. Certification and regulatory requirements are application-specific and should be confirmed with current documentation for the order. These leaded grades are not lead-free alloys. If restrictions apply to the destination or finished equipment, include them in the enquiry so material selection and compliance evidence can be reviewed.
Why choose Brass Parts India
Brass Parts India provides a focused source for custom brass and copper component enquiries from Jamnagar, India. Its turned-parts range includes drawing-based manufacture, multiple thread families and natural or plated finishes. Buyers can discuss the required component geometry together with related turned and pressed parts in the same product category. This is useful when one assembly contains several small components with different manufacturing routes.
The practical basis for supplier selection is a clear quotation, an agreed drawing and appropriate evidence of conformity. Send the functional requirements early so material, finish and inspection can be coordinated. For an OEM programme, identify expected repeat quantities and approval samples. For project procurement, include destination and delivery milestones. For distribution, specify stock labels and packaging. The quotation should state the confirmed supply scope and any unresolved technical points before the order is placed.
Frequently asked questions
Is CW614N the same as CuZn39Pb3?
CW614N is the European material number associated with CuZn39Pb3. CZ121Pb3 is a common legacy cross-reference. The ordered product standard and temper still govern acceptance, so a commercial grade comparison cannot replace a review of the purchase specification.
What information is needed for a quotation?
Send a dimensioned drawing, material standard, quantity, finish and delivery destination. Include the drawing revision, critical tolerances, required inspection documents and intended application. If only a sample is available, identify which characteristics must be reverse-engineered and which material requirements are already known.
Is the listed rate per part or per kilogram?
The displayed rate is US$ 13.90/kg. A kilogram rate is different from a unit price. Provide the finished-part weight and order quantity so the quotation can state the applicable weight basis, tooling, finishing, packing, freight and taxes clearly before purchase.
Can I order a custom thread or non-standard geometry?
Submit the complete thread callout and component drawing for review. Custom shoulders, slots, cross holes, knurls and bores need dimensional and inspection requirements. Manufacturing feasibility depends on the geometry, stock form and quantity; acceptance is confirmed in the quotation.
Are international equivalents automatically interchangeable?
No. A cross-reference is a starting point for material review. Compare the ordered standards, composition limits, temper, product form and mechanical properties. A substitute should be accepted in writing before production, especially when the part belongs to a controlled OEM design.
Can these parts be used in electrical equipment?
They can be considered for suitable electrical component designs. Current rating, temperature rise, conductor retention, contact resistance and insulation clearances are properties of the complete assembly. The equipment designer must establish those requirements and validate the finished configuration where necessary.
Are these alloys lead-free or automatically compliant?
These are leaded brass families. Do not describe them as lead-free. Regulatory conformity depends on the application, destination, applicable rules and any valid exemption. Request current material and compliance documentation for the specific order; a generic alloy designation is not a compliance certificate.
What tolerances and surface roughness are available?
Dimensions and roughness are agreed against the drawing after manufacturing review. There is no universal tolerance or finish applicable to every component in this range. Identify functional surfaces and final dimensions after plating so inspection measures the condition the assembly actually requires.
Can inspection reports or material certificates be supplied?
Specify the required records at enquiry stage, including material certification, dimensional reports and any special tests. The quotation should confirm the agreed scope and document format. A raw-material certificate and a finished-part inspection report cover different aspects of conformity.
How do I arrange repeat orders?
Quote the approved part number, drawing revision, material, finish and previous order reference. State the next batch quantity and delivery requirement. Any design, material or finish change should be reviewed before release so the next batch remains compatible with the approved assembly.
Equivalent product terms in other languages
Use these purchasing terms with the grade CW614N. They translate component descriptions, not material specifications.
| Language | Related product terms |
|---|---|
| Spanish | piezas torneadas de latón; componentes de latón mecanizados; casquillos de latón |
| Russian | токарные детали из латуни; механически обработанные латунные детали; латунные втулки |
| French | pièces décolletées en laiton; composants en laiton usinés; douilles en laiton |
| Portuguese | peças torneadas de latão; componentes de latão usinados; buchas de latão |
| Italian | particolari torniti in ottone; componenti in ottone lavorati; boccole in ottone |
Linked parts and related terms
Explore existing products in the same turned-and-pressed-parts category when preparing an assembly enquiry:
- Brass turned components and precision turned parts
- Brass screw machine parts and threaded components
- Brass pressed parts
- Brass and copper pressings
- Brass washers and copper washers
- Washers and pressed components
Request a CW614N component quotation
US$ 13.90/kg
Send your drawing, quantity, required material standard, finish and inspection requirements to Brass Parts India. Include the delivery country and any approved substitute grades. Our enquiry review can then address manufacturing feasibility and the commercial scope for your component.
Request a quote for CW614N parts
Sales: sales@brass-parts-india.com · +91 22 43 44 9300
Plot 10, GIDC Industrial Estate, Shanker Tekri, Udyog Nagar, Jamnagar 361004, India.
Sales enquiries: India and international export markets.